
01
CDO-WD1 Single-Die Wire Drawing Machine
A flexible pass-by-pass model for frequent diameter changes, shorter batches and direct operator control over each drawing reduction.
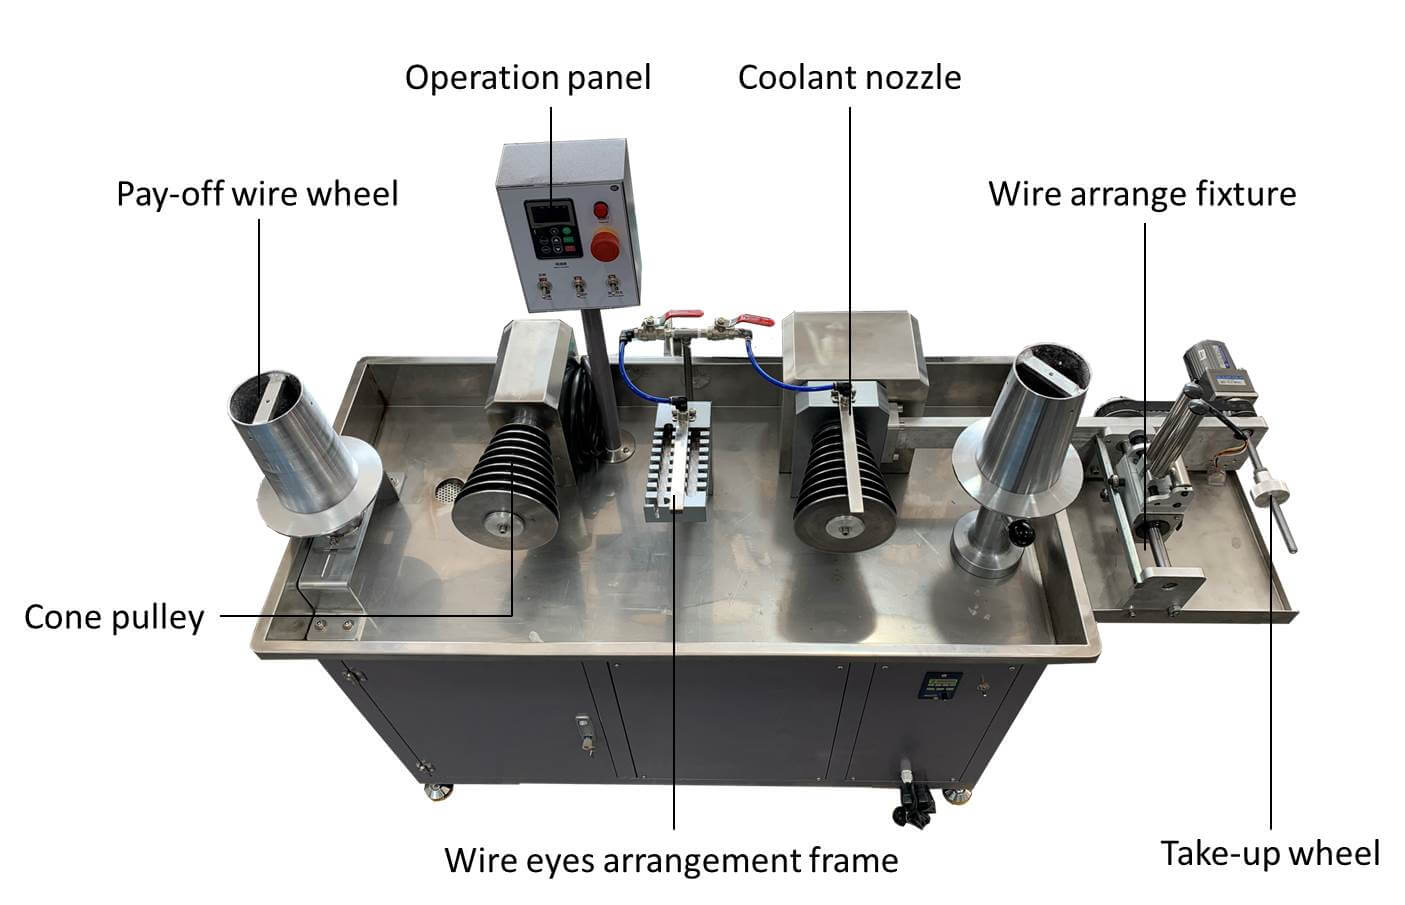
Die1 die
Wire range2.2–0.2 mm
Speed0–50 m/min
 cdocast
Buy the most advanced wire drawing machine to draw your own size wire. Inquiry Now.
CDOCAST supplies single-die, 8-die, 12-die, one-way, two-way and horizontal numerical-control wire drawing machines. The complete series covers fine wire production down to the listed 0.2 mm range and larger incoming wire up to 12 mm.

A wire drawing machine pulls metal wire through one or more progressively smaller dies. Each pass reduces the cross-sectional area and increases the wire length, producing controlled diameters for jewelry chain, findings, electrical parts, brazing wire and other precision products.
For gold and silver wire drawing, the machine is only one part of the process. The incoming rod must be suitable for the first die, the die sequence must avoid excessive reduction, and the alloy may require intermediate annealing as work hardening increases. Lubrication, cooling, take-up control and correct die alignment help protect the surface and stabilize the finished size.
All models belong to one CDOCAST wire drawing machine series. Model suffixes identify the structure: H for horizontal, O for one-way and T for two-way.
A flexible pass-by-pass model for frequent diameter changes, shorter batches and direct operator control over each drawing reduction.

Horizontal drawing configuration for wire up to 8 mm, with an 86×86 stepper motor and controller plus a PP magnetic pump for the cooling circuit.

The one-way model handles wire up to 2 mm and uses a chrome-plated 45# steel take-up reel hardened to HRC 60–62.

The two-way configuration handles wire up to 4 mm with hardened chrome-plated 45# steel take-up reels.

A larger two-way configuration for wire up to 8 mm, with HRC 60–62 chrome-plated 45# steel take-up reels.

The largest listed two-way model handles wire up to 12 mm with an 11 kW motor and a published drawing speed of 20 m/min.

Eight progressive die positions support repeat production where several reductions are needed between the prepared wire and finished fine wire.
A progressive 12-die machine with a listed 1.5–0.2 mm wire-size range, 89 m/min drawing speed and Cr12MoV drawing cones at HRC 60–62.
All models are compared in one table. A dash means the value is not stated in the available published specification.
| Model | Size (L×W×H) | Weight | Motor | Voltage | Wire range | Drawing speed | Drawing / take-up system |
|---|---|---|---|---|---|---|---|
| CDO-WD1 Single-Die | 650×550×1000 mm | 150 kg | 4 kW | 3 phase 380 V, 50/60 Hz | 2.2–0.2 mm | 0–50 m/min | 1 die; automatic liquid cooling |
| CDO-WD-H8 Horizontal Numerical Control | 1200×1400×1370 mm | 900 kg | 5.5 kW | 3 phase 380 V | ≤8 mm | — | 86×86 stepper motor; PP magnetic cooling pump |
| CDO-WD-O2 One-Way | 1500×750×1260 mm | 600 kg | 5.5 kW | 3 phase 380 V | ≤2 mm | 32 m/min | 45# steel chrome-plated reel; HRC 60–62 |
| CDO-WD-T4 Two-Way | 1700×750×1260 mm | 700 kg | 3 kW | 3 phase 380 V | ≤4 mm | 21 m/min | 45# steel chrome-plated reels; HRC 60–62 |
| CDO-WD-T8 Two-Way | 1900×800×1400 mm | 900 kg | 5.5 kW | 3 phase 380 V | ≤8 mm | 32 m/min | 45# steel chrome-plated reels; HRC 60–62 |
| CDO-WD-T12 Two-Way | 1900×1520×1340 mm | 2000 kg | 11 kW | 3 phase 380 V | ≤12 mm | 20 m/min | 45# steel chrome-plated reels; HRC 60–62 |
| CDO-WD8 Eight-Die | 1300×740×1370 mm | 420 kg | 4 kW | 3 phase 380 V, 50/60 Hz | 2.2–0.2 mm | 0–50 m/min | 8 dies; automatic liquid cooling |
| CDO-WD12 Twelve-Die | 1700×780×1360 mm | 550 kg | 4 kW | 3 phase 380 V | 1.5–0.2 mm | 89 m/min | 12 dies; Cr12MoV drawing cones; HRC 60–62 |
“One-way” and “two-way” identify the published machine structures. Confirm the required wire path, die schedule, pay-off and take-up arrangement before ordering.
A stable result depends on a complete reduction plan, not only the machine's maximum diameter or speed.
Roll or cast the feedstock to a suitable, clean and dimensionally consistent starting diameter.
Reduce the leading end so it can pass through the first die and be gripped by the take-up system.
Use the approved die sequence, drawing lubricant, cooling flow and speed for the selected alloy.
Restore ductility between reductions when work hardening would otherwise cause cracking or excessive drawing force.
Verify diameter, surface, roundness and coil condition before the next pass or downstream production.
Different structures solve different production problems; the highest die count is not automatically the best choice.
These details allow the manufacturer to check the drawing route instead of recommending a machine from wire diameter alone.
Internal links connect the drawing machine with upstream sizing, end preparation and intermediate heat treatment.
Practical purchasing questions for gold, silver, copper and jewelry wire manufacturers.
The published applications include gold, silver and copper wire. Compatible alloys may also be processed, but die material, lubrication, reduction per pass, speed and annealing schedule should be selected for the actual alloy rather than assumed from the base metal.
CDO-WD1 and CDO-WD8 list a 2.2–0.2 mm range, while the 12-die model lists a 1.5–0.2 mm range. Achieving stable 0.2 mm wire depends on correct feed preparation, die sequence, wire condition, lubrication and operator setup.
Choose a single-die machine for flexible pass-by-pass work, frequent product changes and smaller batches. Choose an 8- or 12-die machine when repeat production requires several progressive reductions and a more integrated wire path.
Wire drawing pulls material through a die to reduce and size it. Wire rolling compresses material between rolls and is often used upstream to prepare rod or shaped wire before the final drawing passes.
Cold drawing work-hardens many gold, silver, copper and alloy wires. Intermediate annealing restores ductility when the accumulated reduction would otherwise increase force, damage the surface or cause cracking. The required interval depends on the alloy and pass schedule.
The series includes one-way and two-way configurations for incoming wire up to 2, 4, 8 and 12 mm, plus a horizontal numerical-control configuration up to 8 mm. Selection also depends on coil weight, target output, required speed and reduction plan.
Provide the metal and alloy, incoming and final diameter, intermediate pass sizes if available, finished tolerance, coil weight, target output, annealing plan, factory voltage and preferred pay-off and take-up arrangement.
Send CDOCAST your input diameter, final wire size, alloy, coil weight and output target for suitable die, drawing and take-up configuration selection.