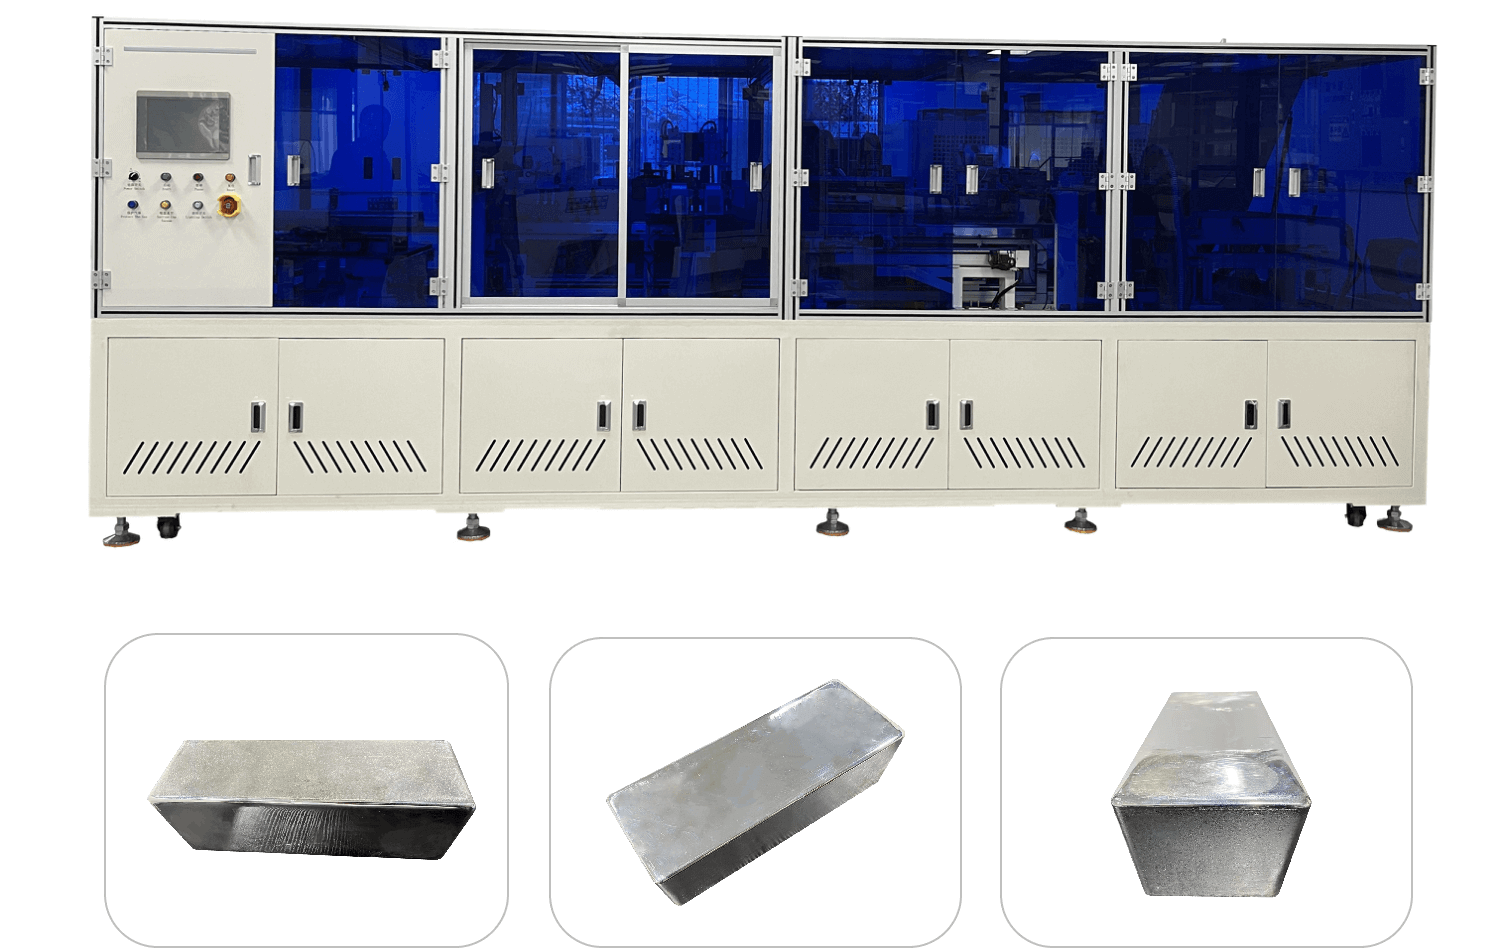
Compact Automatic-Lid Model
CDO-F1 · 1 kg
For small bullion workshops, jewelry factories and assay operations producing 1 kg gold bars or trial batches. Compact chamber and convenient mold handling.
25 kW1 × 1 kgsmall footprint
Watch CDO-F1 video → cdocast
The most popular vacuum gold bar making machine for sale, Inquiry Now!
CDOCAST vacuum gold bar making machines combine induction heating, a controlled vacuum chamber, inert-gas protection and a matched graphite mold. Six configurations support compact 1 kg gold bars, multi-bar production, 12.5 kg ingots and 1000 oz silver bars.
This is the core casting machine in a complete gold and silver bar production line. A practical line may also require a correctly sized water chiller, metal granulator, hydraulic logo stamping press, custom dies and a dot peen marking machine for variable serial numbers.
 Watch Vacuum Gold Bar Casting YouTube ↗
The same nominal capacity can be arranged as one larger bar or several smaller bars only when the chamber and custom graphite mold support that layout.
For small bullion workshops, jewelry factories and assay operations producing 1 kg gold bars or trial batches. Compact chamber and convenient mold handling.

A cost-balanced choice for one 2 kg bar or a supported two-cavity 1 kg layout. Suitable for bullion dealers, recycling shops and smaller refineries.

Designed for higher output than compact machines. It can be configured for four 1 kg bars and is often the practical starting point for regular silver bullion production.

For refineries and bullion factories that need eight supported bar cavities in one cycle and want to reduce repeated loading, heating and cooling operations.

For 12.5 kg gold or silver ingots. Heavy mold operation should be quoted together with the correct graphite mold, mold frame and suitable lifting or handling method.

For heavy silver bullion and 1000 oz silver bars. The quotation should include confirmed bar drawings, cooling load, workshop access and safe mold transfer equipment.
Use this table for model comparison. Final mold arrangement and actual cycle must be confirmed against the customer's finished bar.
| Model | Power supply | Power | Standard gold layout | Approx. melting | Approx. cooling | Machine size (mm) |
|---|---|---|---|---|---|---|
| CDO-F1 | 3 phase, 380 V | 25 kW | 1 × 1 kg | 5–7 min | 6–7 min | 950 × 750 × 1070 |
| CDO-F2 | 3 phase, 380 V | 35 kW | 2 × 1 kg | 6–8 min | 7–8 min | 1100 × 880 × 1100 |
| CDO-F4 | 3 phase, 380 V | 45 kW | 4 × 1 kg | 7–8 min | 7–10 min | 1520 × 900 × 1080 |
| CDO-F8 | 3 phase, 380 V | 75 kW | 8 × 1 kg | 11–15 min | 12–16 min | 1530 × 650 × 980 |
| CDO-F12 | 3 phase, 380 V | 75 kW | 1 × 12.5 kg | 10–14 min | 11–15 min | 1680 × 780 × 1120 |
| CDO-F30 | 3 phase, 380 V | 90 kW | 1 × 30 kg | 15–17 min | 14–16 min | 1700 × 960 × 1600 |
Cycle time is an estimate, not guaranteed output. It changes with metal type and purity, starting temperature, bar thickness, graphite mold design, chamber settings, cooling-water temperature and chiller performance. Power supply can be engineered for the destination where technically available; confirm voltage, phase and frequency before ordering.
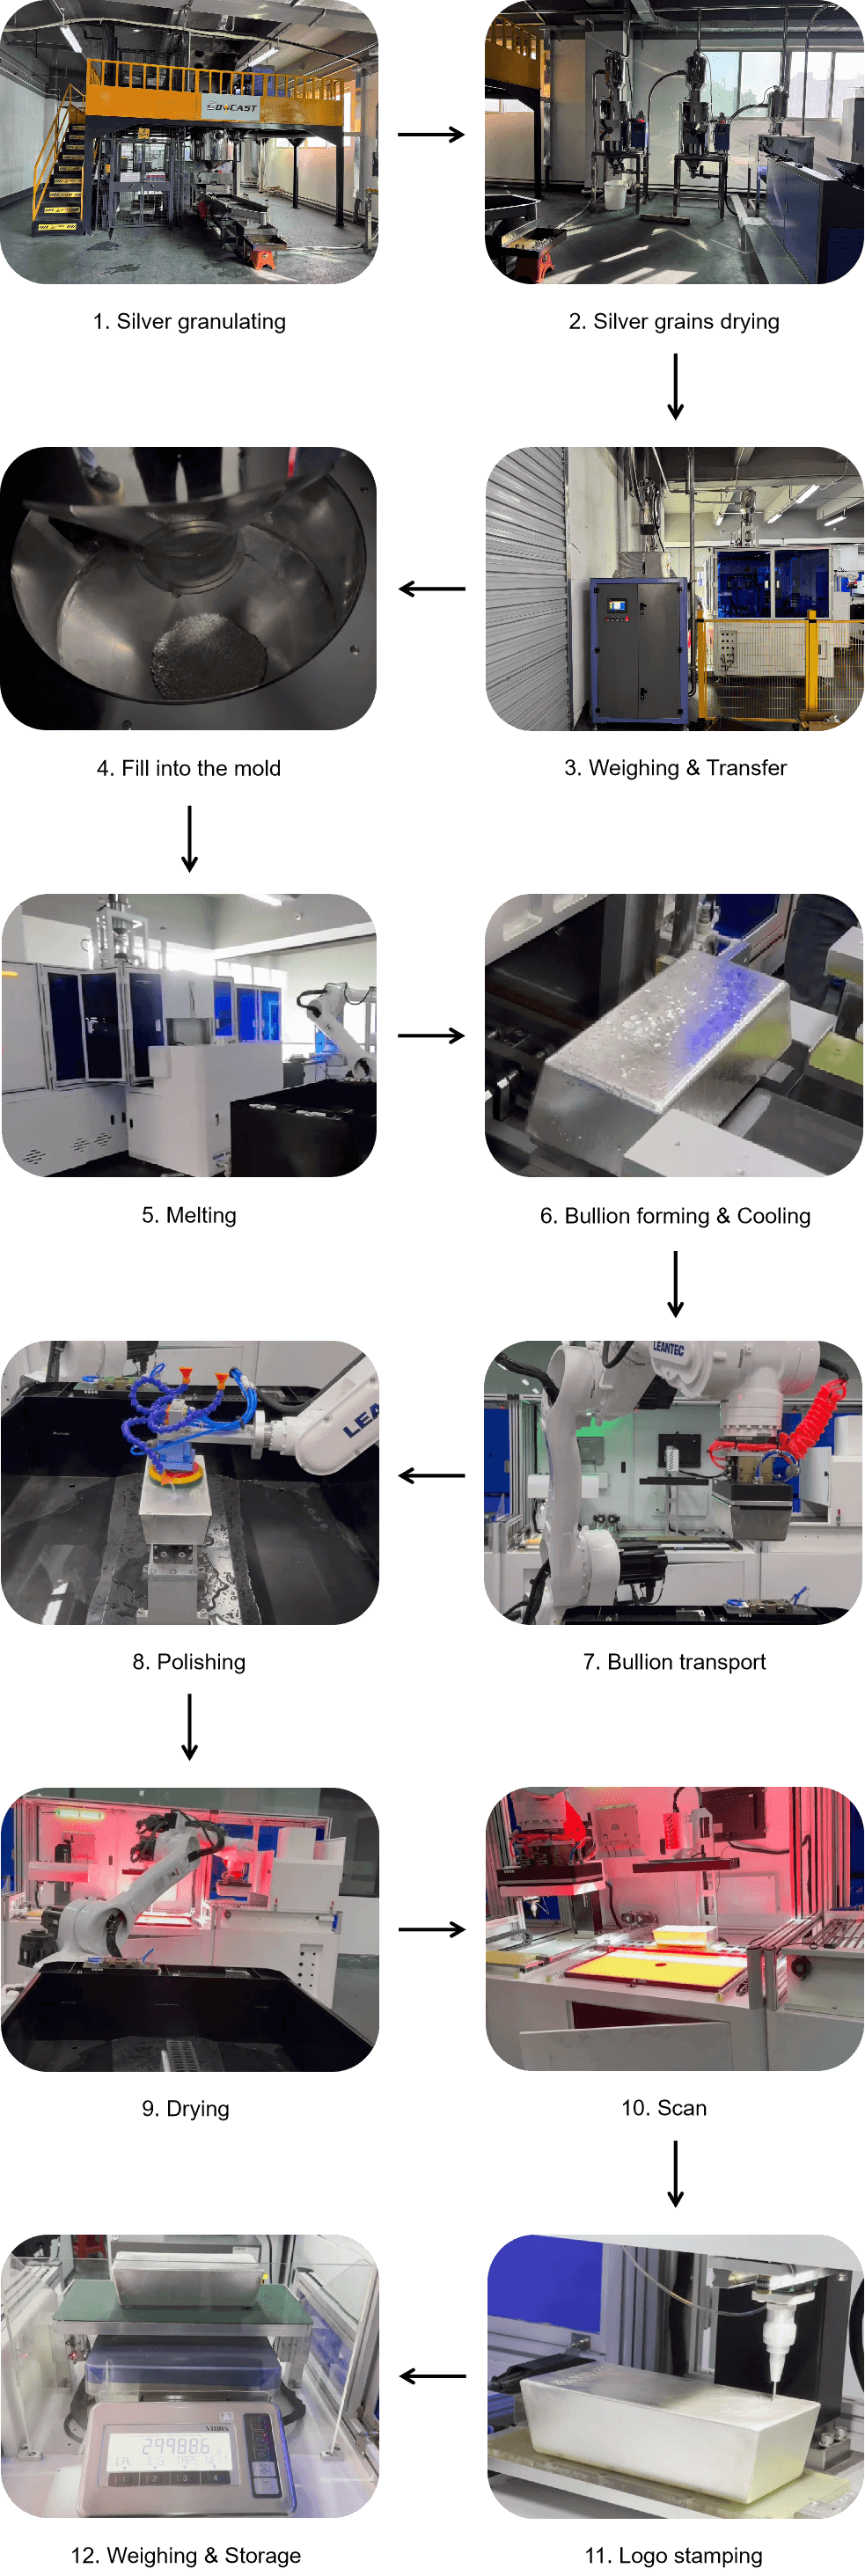
This workflow shows where the main machine and each supporting machine are used.
Use clean refined metal. A granulator is useful when large material must be converted into uniform, easy-to-weigh grains.
Weigh material for the required finished bar and loading allowance according to the approved production procedure.
Use a custom mold matching the confirmed bar weight, length, width, thickness and cavity layout.
The chamber is evacuated and the approved inert-gas settings are used to control the casting environment.
The metal is melted inside the matched mold rather than manually poured from an open crucible.
The water chiller maintains the required cooling-water conditions for the induction system and casting cycle.
A hydraulic press and custom die apply the brand logo, purity, weight or other repeatable deep marks.
A dot peen marking machine adds changing serial numbers, batch codes or traceability characters after casting.
A vacuum gold bar casting machine provides the controlled environment, but the final mirror-like surface also depends on the material, graphite mold, vacuum integrity, heating profile and cooling conditions.
Purity, alloy composition, moisture, flux residue and contamination can all change color and surface reflection. Confirm the feed material before changing machine parameters.
Match the cavity to the bar dimensions and use dense, clean and dry graphite. Inspect the mold for oxidation, powder shedding, cracks or residue before loading valuable metal.
Preheat according to the approved process so the mold is not too cold or overheated. Excessive heating accelerates graphite oxidation, while unstable mold temperature can affect solidification.
Check chamber seals, vacuum lines, pump condition and the specified argon or nitrogen program. Pinholes and oxidation marks should be diagnosed before simply increasing heating time.
Set melting and cooling time for the metal, bar thickness and mold layout. A correctly sized water chiller helps keep cooling-water temperature and flow consistent from batch to batch.
Dull film, graphite adhesion, ripple marks, shrinkage and pinholes have different causes. Record the material batch, mold condition, vacuum value and cycle settings before making one controlled adjustment.
“Required” means the production utility or tooling is necessary. “Recommended option” depends on the customer's incoming material and marking requirement.
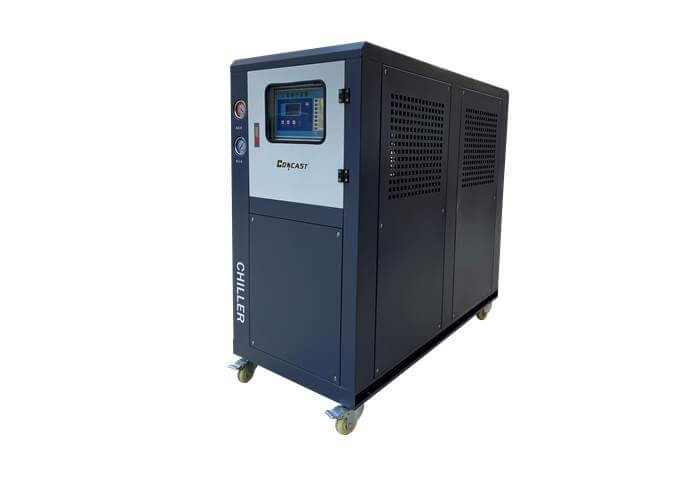
Provides stable circulating water for the induction power system and casting process. Chiller capacity must be matched to the selected CDO-F model, ambient temperature, water flow, inlet temperature and operating hours—not selected only by appearance or tank size.
View water chiller →
The graphite mold determines the finished bar cavity, dimensions and number of bars per cycle. CDOCAST can machine molds for gold and silver bars according to the customer's required weight and drawing. Before production, confirm the bar length, width, thickness, side taper, corner radius, top and bottom shape, cavity quantity and any handling structure required by the selected CDO-F machine.
View custom graphite molds →
Converts refined metal into smaller grains that are easier to weigh and distribute inside the graphite mold. It is especially useful when the incoming material is a large block, irregular scrap or when repeatable charge preparation matters. It does not replace refining or purity control.
Compare metal granulators →
Uses controlled pressing force and a custom positioning die to apply repeatable information such as the refinery logo, purity and nominal weight. Press tonnage and die structure should be selected from the bar footprint, metal, mark depth and production frequency.
Choose a logo stamping press →
A computer-controlled marking pin creates permanent dot-matrix characters on the bar surface. It is the practical choice for information that changes on every bar, such as serial numbers, batch codes and production identifiers. Confirm marking area, character height, depth and whether compressed air is available.
See the complete bar-making process →Professional bullion producers commonly use both because the information and marking method are different.
Best for fixed information and a stronger pressed impression.
Best for variable information that changes from bar to bar.
These are purchasing frameworks. The final bill of materials is confirmed after reviewing the finished bar drawing and workshop utilities.
For small batches, custom bullion and moderate daily output.
For regular gold and silver bar production with stronger throughput.
For standard-size heavy ingots and 1000 oz silver bars.
A clear inquiry reduces repeated emails and prevents the wrong mold, chiller or marking system from being quoted.
Important: If an existing chiller will be reused, send its cooling capacity, water flow, pump pressure, tank volume and operating temperature—not only its model name.
These short guides help buyers understand the product type, expected bar surface, mold relationship and downstream process before confirming a machine.

Learn how graphite powder, porosity, rough black dots, incomplete melting and vibration marks are diagnosed.
Mirror FinishWhat causes a dull gold bar surface?Understand the effects of mold condition, raw material cleanliness, process settings and cooling on surface reflection.
Machine DifferenceMelting furnace or vacuum bar casting machine?Compare open melting and manual pouring with controlled vacuum bullion casting before selecting equipment.
Product RouteCast bar or minted bar production?See why casting bars and minted bars require different forming, rolling, blanking, polishing and stamping equipment.
Complete ProcessHow is a finished gold bullion bar produced?Follow material preparation, vacuum casting, logo pressing and serial-number marking as one connected workflow.
Custom ToolingHow should a graphite bar mold be specified?Review graphite selection and prepare the bar drawing, cavity size and mold details needed for customization.
Keep only this visible FAQ on the page. If Rank Math FAQ schema is used, enter the same questions and answers there without adding another visible FAQ block.
Send the metal, purity, bar weight and dimensions, bars per cycle, daily output, logo artwork, serial-number format, local power supply and available workshop utilities. CDOCAST can then quote the correct vacuum casting machine, graphite molds, water chiller, granulator, hydraulic logo press and dot peen marking system.


Click here to watch the video»


Click here to watch the video»

 8KG Vacuum Gold Bar Making Machine with Auto Lid Opening


Click here to watch the video»

 Tunnel Furnace for Automatic Vacuum Casting 1000oz 30Kg Silver Bullion
Click here to watch the video»