Which metals are suitable for an upward continuous casting machine?
The published applications include pure copper, approved oxygen-controlled copper grades, brass, bronze, silver, gold, K-gold and other compatible nonferrous alloys. Provide the exact composition with the inquiry because melting behavior, oxidation protection, crystallizer design, temperature and traction settings vary by alloy.
What products can the upward continuous casting machine manufacture?
The machine can be configured for approved solid rods, wire-drawing feedstock, bars, tubes and plate or strip sections. Each product requires a suitable crystallizer, starting tool, traction arrangement and process setting; one generic mould cannot cover every shape and size.
What product sizes can the small upward casting machine produce?
The existing CDOCAST page publishes typical ranges of Φ6–30 mm for silver or copper rod, OD 20–80 mm for tube with wall thickness linked to diameter, and 12–40 mm width by 6–12 mm thickness for plate or strip. These are reference ranges rather than universal guarantees. Confirm the alloy, finished drawing, tolerance, strand quantity and required output before the crystallizer is designed.
How does an upward continuous casting machine work?
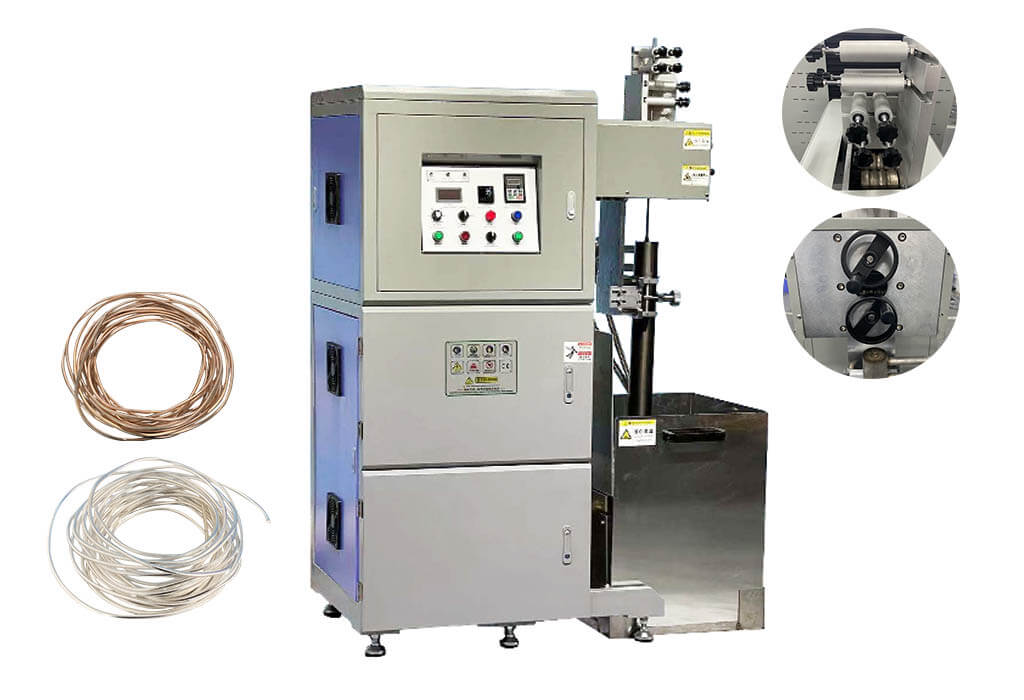
Metal is melted in the induction-heated crucible. A water-cooled crystallizer removes heat locally from the molten bath, forming a solid shell. The servo traction mechanism then pulls the strand upward according to the approved pull distance, pause time and speed, creating a continuous or semi-continuous product.
How can metal oxidation be reduced during upward casting?
Oxidation control depends on the metal and required quality. For copper, the existing process uses an approved charcoal or graphite-flake melt cover to reduce direct contact with the furnace atmosphere. Precious metals or sensitive alloys may require a different protective method. All charging tools and materials must remain clean and completely dry.
What are the main consumables and how long do they last?
Typical consumables include the silicon-carbide graphite crucible, graphite mould or crystallizer components, insulation and starting components. The original page gives reference service-life figures, but actual life changes significantly with alloy, operating temperature, thermal cycling, protection practice, cooling-water condition and maintenance. Consumable life should therefore be treated as an operating estimate rather than a guaranteed number of heats or tons.
How do I select the correct upward continuous casting machine?
Provide the metal composition, finished product drawing and tolerance, daily output, operating hours, strand quantity, coil or cut-length requirement and downstream process. CDO-UP45 is rated for 50 kg of copper, while CDO-UP70 is rated for 100 kg. The larger capacity is useful only when it matches the required section, crystallizer, production schedule and factory utilities.
What are the advantages of upward casting compared with horizontal continuous casting?
The integrated small upward caster offers a compact layout, flexible campaign production and convenient changes between approved crystallizers. Upward withdrawal can also simplify strand collection for rod and wire-feedstock applications. Neither direction is automatically superior: horizontal casting may better suit some bar, strip or high-output layouts, so the decision should be based on alloy, section, output, quality target and downstream handling.
Why does the crystallizer need a separate cooling-water circuit?
The crystallizer must remove heat at a controlled rate so the strand develops a stable shell before upward withdrawal. Clean, stable cooling helps control surface quality, structure and breakout risk. Scale, blocked passages, unstable flow or water leakage can create serious quality and safety problems. Use the water quality, temperature, pressure and flow stated in the approved technical proposal rather than applying one setting to every product.
Are casting speed and cooling intensity adjustable, and how do they affect quality?
Yes. Traction speed, pull distance, pause time and cooling conditions are adjusted for the alloy and section. Pulling too fast or cooling too weak can leave an insufficient solid shell, increasing the risk of leakage, porosity or shrinkage defects. An unsuitable slow cycle or excessive cooling can increase friction, thermal stress, cracking and production time. The published 1000 mm/min drawing speed is a machine reference value, not guaranteed output for every product.
What safety precautions are required when operating the machine?
Operators need suitable high-temperature protective clothing, gloves and face protection. Electrical equipment must be grounded, cooling circuits must be inspected for leakage, and water must never contact molten metal. Charges, tools and additives must be dry. Regularly inspect the crucible, crystallizer, graphite parts, traction mechanism and cooling passages, and follow the supplied operating and emergency procedures.