
Precious Metal Coins, Ingots, and Strips
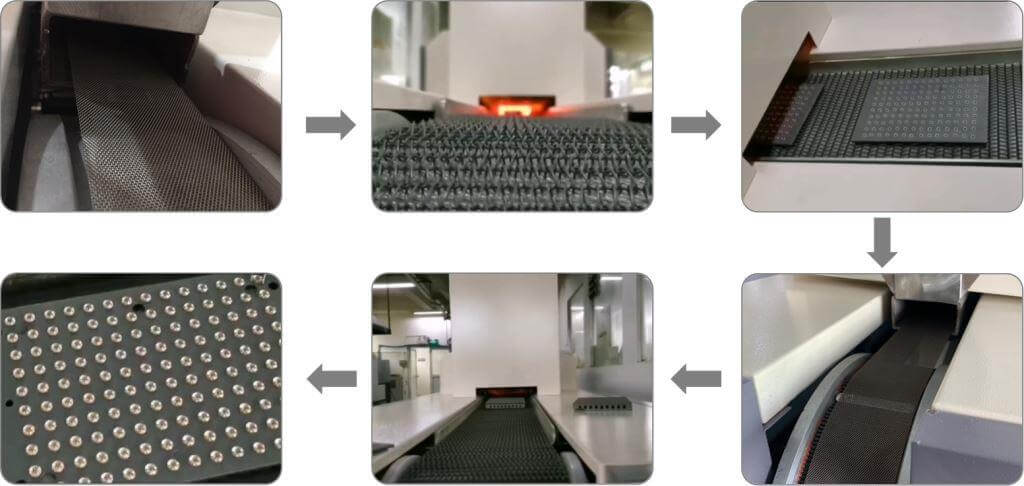
Used for bright annealing of gold, silver, platinum, and other precious metal products before further forming, stamping, or finishing.
 cdocast
Purchase the most ecomonical Mesh belt heat treatment furnace in china!
Continuous Annealing and Welding Furnace
CDOCAST mesh belt heat treatment furnace is designed for continuous annealing, bright annealing, brazing, and welding of metal strips, precious metal coins, ingots, jewelry chains, copper parts, stainless steel parts, and small metal components under a controlled protective atmosphere.
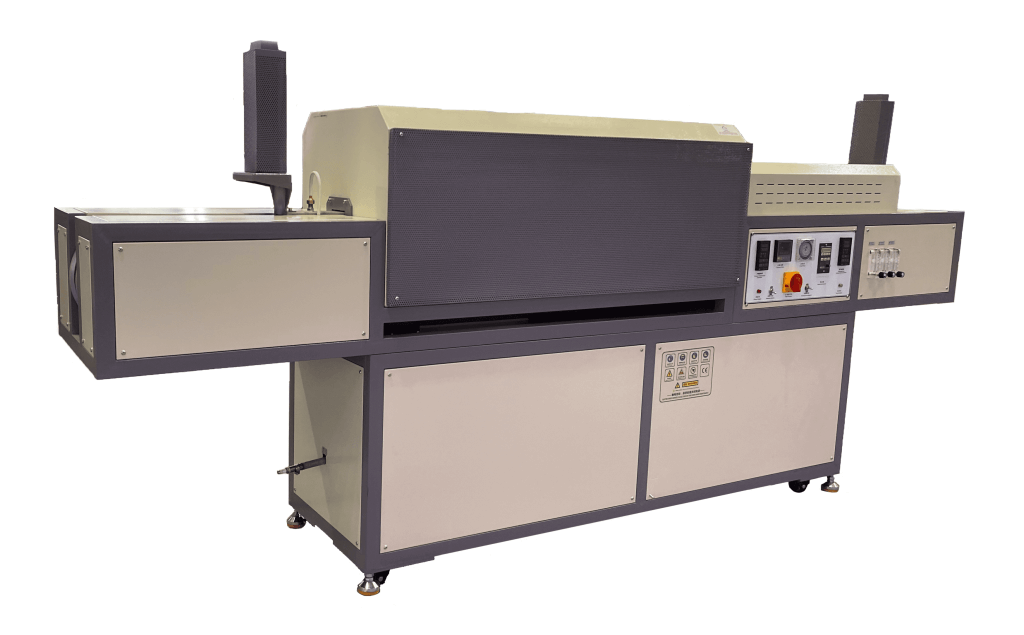
Understand the working principle before choosing furnace length, belt width, atmosphere control, and production output.
A mesh belt heat treatment furnace is a continuous heat treatment oven that uses a moving mesh belt to carry metal workpieces through heating, protective atmosphere, and cooling zones. It is commonly used as a mesh belt annealing furnace, continuous annealing furnace, bright annealing furnace, and mesh belt brazing furnace when factories need stable temperature, automatic discharge, and reduced surface oxidation.
This structure is designed for buyers who need more stable continuous annealing, stronger furnace capacity, and better process control during long production runs.
A double chamber annealing furnace gives the production line more room for heating control, atmosphere protection, and stable residence time. It can be equipped with an ammonia dissociation system, or configured with gas flow control to introduce nitrogen and hydrogen in the required ratio for bright annealing and oxidation control.
This heavy duty mesh belt annealing furnace is suitable for factories processing metal strips, jewelry parts, copper components, screws, rods, and precision parts in larger batches.
Different products require different belt widths, temperature settings, atmosphere control, and cooling conditions.
Used for bright annealing of gold, silver, platinum, and other precious metal products before further forming, stamping, or finishing.
Suitable for continuous jewelry welding furnace applications where small workpieces need stable heating and controlled surface brightness.
Supports copper strip annealing, copper bar heat treatment, and small copper part bright annealing with protective gas control.
Used for screws, sockets, chains, rods, wire parts, and other small components requiring continuous heat treatment.
Protective atmosphere furnace design helps reduce oxidation and maintain a brighter product surface after annealing or brazing.
Continuous mesh belt transfer is useful when the factory needs stable output, repeatable process parameters, and lower labor cost.
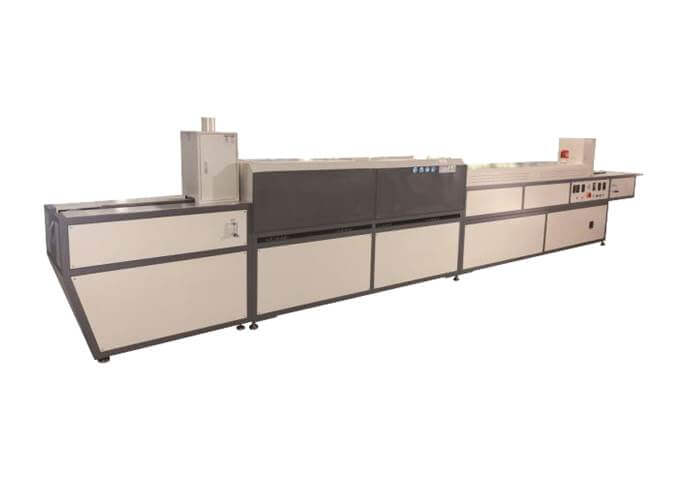
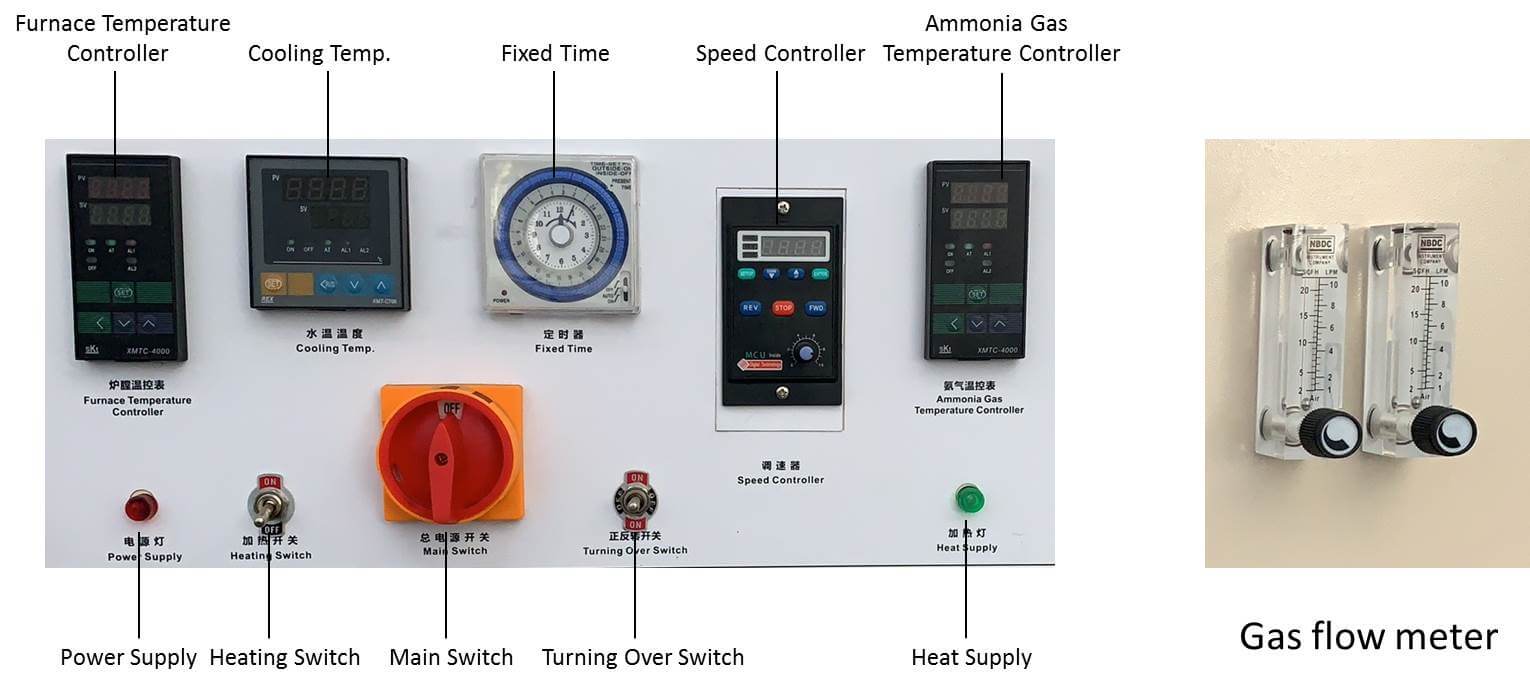
These images show common CDOCAST mesh belt furnace structures, furnace details, and application examples.
For oxidation-sensitive products, the furnace atmosphere is as important as the heating temperature.
| System | How It Works | Buyer Benefit |
|---|---|---|
| Ammonia Dissociator | Ammonia is decomposed into nitrogen and hydrogen for protective atmosphere control. | Helps create an oxidation-reducing environment for bright annealing. |
| Nitrogen Protection | Nitrogen helps isolate oxygen from the furnace chamber during heat treatment. | Reduces oxidation risk on metal surfaces during continuous annealing. |
| Hydrogen Reduction | Hydrogen can help reduce oxide layers formed on the workpiece surface. | Supports brighter surface results for precious metals, copper, and suitable alloys. |
| Burner and Exhaust Treatment | Burners at inlet and outlet help consume oxygen and handle exhaust gases. | Improves atmosphere stability and operating safety. |
| Graphite Seals | Graphite sealing at inlet and outlet reduces rapid gas escape. | Keeps the protective atmosphere more stable inside the furnace. |
The right mesh belt furnace model depends on material, part size, temperature, belt width, atmosphere, and expected daily output.
| Parameter | What to Confirm | Why It Matters |
|---|---|---|
| Workpiece Material | Gold, silver, copper, stainless steel, jewelry alloy, small metal parts | Material affects temperature, atmosphere, belt speed, and cooling design. |
| Workpiece Size | Length, width, thickness, weight, and loading density | Determines mesh belt width, furnace opening height, and residence time. |
| Operating Temperature | Required heating zone temperature and maximum process temperature | High-temperature processes may require custom chamber and heating elements. |
| Mesh Belt Width | Standard and custom belt width options according to output requirement | Belt width affects throughput, product spacing, and overall furnace size. |
| Belt Speed | Adjustable belt speed based on annealing or brazing time | Controls residence time and helps stabilize final product quality. |
| Daily Production Output | Target quantity per hour or per day | Helps engineers recommend furnace length, heating power, and cooling capacity. |
Many buyers compare a continuous mesh belt annealing furnace with a box-type annealing furnace before purchasing.
| Comparison | Mesh Belt Heat Treatment Furnace | Box Annealing Furnace |
|---|---|---|
| Production Method | Continuous feeding and automatic discharge by conveyor belt | Batch loading and unloading by operator |
| Output | Better for large-volume continuous production | Better for small batches or flexible trial production |
| Labor Requirement | Lower manual handling after setup | More manual loading, waiting, and unloading |
| Process Stability | Stable belt speed, temperature zone, and residence time | Depends more on batch size and operator process control |
| Surface Oxidation Control | Can integrate nitrogen and hydrogen protective atmosphere | Can protect parts, but continuous atmosphere control is less efficient for high output |
A correct quotation should be based on the real product and production target, not only a furnace name.
Compare related heat treatment equipment by product type, temperature range, protective atmosphere, and production method.
Send your workpiece material, dimensions, temperature, belt width, and daily output. CDOCAST engineers can recommend a suitable mesh belt heat treatment furnace configuration.
→Click here to watch the video
| Model number | CDO-30MB | CDO-40MB |
| Power source | Three phase 380V±10%, 50/60Hz | Three phase 380V±10%, 50/60Hz |
| Power | 16 kw | 18 kw |
| Max temperature | 1000°C | 1000°C |
| Applicable metal | All metals | All metals |
| Heating rate | 700°C/80min | 700°C/80min |
| Ammonia decomposition heating time | 880°C/80min | 880°C/80min |
| Welding speed | 1m/min | 1m/min |
| Dimension | 3130(L)*550(W)*1448(H)mm | 3970(L)*550(W)*1448(H)mm |
| Weight | 400kg | 480 kg |
| More models can be customized | ||
1: CDOCAST’S standard length of the tunnel mesh belt heat treatment furnace is 3 meters and 4 meters, and different lengths can also be customized according to customer requirement.
2: PID temperature control program design, Multiple temperature heating curves can be set
3: The high qulity mesh belt imported from Switzerland is used as the conveying device, which has a longer service life than other supplier
4: CDOCAST mesh belt heat treatment furnace comes with ammonia decomposition device, which can automatically decompose ammonia into nitrogen and hydrogen, nitrogen is used for protection, and hydrogen is used for reduction
5: The highest temperature can reach 1000 degrees, and the heating temperature is uniform
6: The speed of the mesh belt can be adjusted, the moving speed of the mesh belt can be adjusted according to different heating processes through the governor
7: A timer is installed in the power control panel, which can be set to heat regularly, which is convenient for users
A: Please provide the following details about the workpiece:
Material for heat treatment/Dimensions/Operating temperature in the heating zone/Mesh belt width/Daily production output
Our standard belt width is 60 mm
A: First, the furnace is equipped with an ammonia dissociator. Inside the furnace, ammonia is thermally decomposed into a mixed atmosphere of nitrogen and hydrogen. Nitrogen acts as an oxygen barrier, while hydrogen reduces any oxide layer that may have formed on the metal surface, restoring its brightness.
Second, a burner is installed at the furnace inlet. These consume oxygen before it enters the chamber. Additionally, the burner at the furnace outlet treat exhaust gases (hydrogen).
Third, graphite seals are used at both the inlet and outlet to prevent rapid escape of nitrogen and hydrogen.
Fourth, graphite sleeves are designed to cover portions of the strip material, protecting its surface from oxidation.
A: The equipment includes an ammonia dissociation temperature controller, which adjusts the dissociation rate of ammonia by regulating its decomposition temperature, thereby controlling the concentration of hydrogen and nitrogen inside the furnace. Ammonia flow can also be adjusted via a flow meter.
A: Welding of precious metal jewelry
Bright annealing of precious metal coins / ingots / strips
A: The mesh belt furnace allows automatic discharge via the conveyor belt, offering higher automation and suitability for large-volume continuous production. Unlike box furnaces, which require manual unloading, this system is more efficient and less labor-intensive.
A: The operating temperature depends on the user’s specific process. However, if the temperature exceeds 1000°C, a custom high-temperature furnace chamber and heating elements (such as resistance wires) are required, which will increase the cost.
A: The furnace is equipped with a chamber temperature controller and a water-cooling temperature controller. Both the workpiece heating temperature and cooling temperature can be set and controlled by the user.
A: Our engineers will recommend the appropriate belt speed and operating temperature based on your product characteristics and process requirements.
Please provide the following details about the workpiece:
Material for heat treatment/Dimensions/Operating temperature in the heating zone/Mesh belt width/Daily production output
Our standard belt width is 60 mm.
First, the furnace is equipped with an ammonia dissociator. Inside the furnace, ammonia is thermally decomposed into a mixed atmosphere of nitrogen and hydrogen. Nitrogen acts as an oxygen barrier, while hydrogen reduces any oxide layer that may have formed on the metal surface, restoring its brightness.
Second, a burner is installed at the furnace inlet. These consume oxygen before it enters the chamber. Additionally, the burner at the furnace outlet treat exhaust gases (hydrogen).
Third, graphite seals are used at both the inlet and outlet to prevent rapid escape of nitrogen and hydrogen.
Fourth, graphite sleeves are designed to cover portions of the strip material, protecting its surface from oxidation.
The equipment includes an ammonia dissociation temperature controller, which adjusts the dissociation rate of ammonia by regulating its decomposition temperature, thereby controlling the concentration of hydrogen and nitrogen inside the furnace. Ammonia flow can also be adjusted via a flow meter.
Welding of precious metal jewelry
Bright annealing of precious metal coins / ingots / strips
The mesh belt furnace allows automatic discharge via the conveyor belt, offering higher automation and suitability for large-volume continuous production. Unlike box furnaces, which require manual unloading, this system is more efficient and less labor-intensive.
The operating temperature depends on the user’s specific process. However, if the temperature exceeds 1000°C, a custom high-temperature furnace chamber and heating elements (such as resistance wires) are required, which will increase the cost.
The furnace is equipped with a chamber temperature controller and a water-cooling temperature controller. Both the workpiece heating temperature and cooling temperature can be set and controlled by the user.
Our engineers will recommend the appropriate belt speed and operating temperature based on your product characteristics and process requirements.
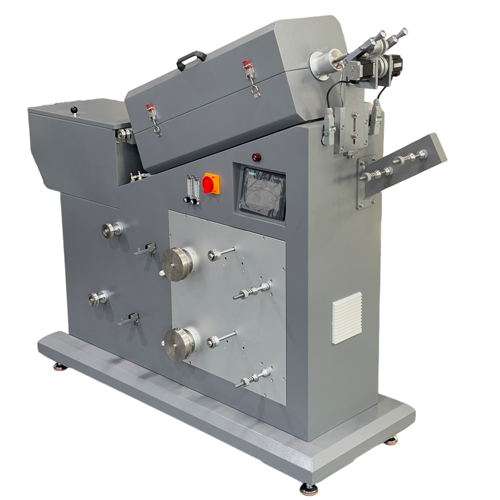 Wire Annealing Furnace
 Annealing Furnace
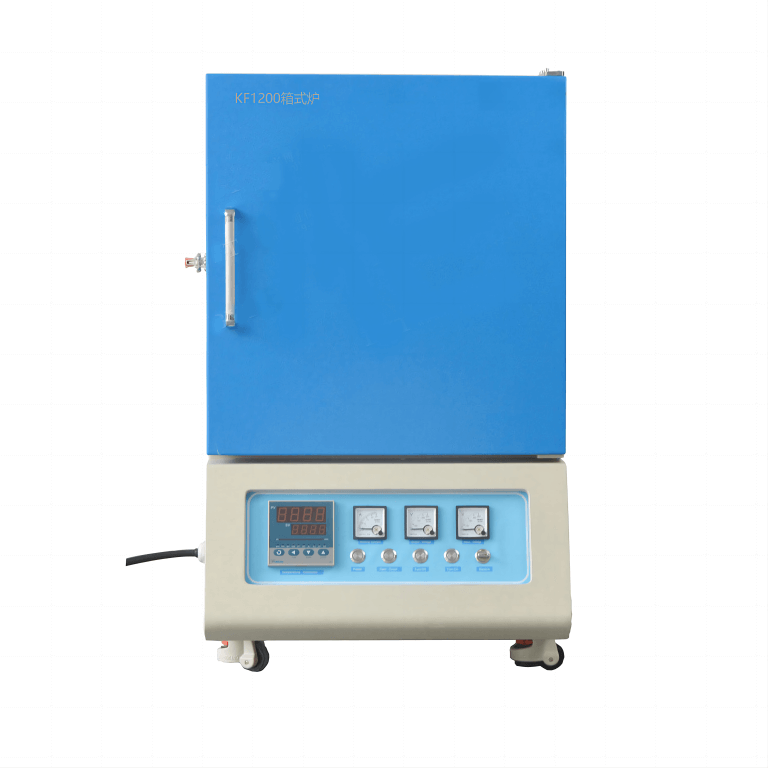 Muffle Furnace