Making gold silver jewelry with jewelry casting equipment

Lost Wax Jewelry Casting Buyer Guide

Jewelry Casting Equipment: Vacuum Pressure vs Centrifugal Casting

Jewelry casting equipment should be selected from the metal, design detail, flask size, batch weight and required casting force. This guide explains when to use vacuum pressure casting for gold and silver, when centrifugal vacuum casting is better for platinum, and which supporting machines are required for a practical lost wax jewelry casting line.

jewelry casting equipment vacuum pressure casting machine centrifugal jewelry casting machine lost wax jewelry casting line
complete jewelry casting equipment line for lost wax gold silver and platinum production

A complete jewelry casting line must coordinate wax patterns, investment preparation, burnout, metal casting, cooling and finishing—not only the casting machine.

Which jewelry casting equipment should you choose?

Choose a vacuum pressure jewelry casting machine for most gold, karat gold, silver and copper-alloy lost wax casting. Vacuum removes air around the flask and controlled gas pressure helps metal fill fine investment cavities. Choose a vacuum centrifugal casting machine for platinum, palladium, stainless steel and other high-temperature, lower-fluidity metals where centrifugal force and a higher-temperature melting system are required. Confirm the exact alloy, flask, casting weight and design thickness with a sample test before ordering. This guide focuses on choosing the casting method and equipment configuration; the linked operation guides cover the step-by-step production workflow.

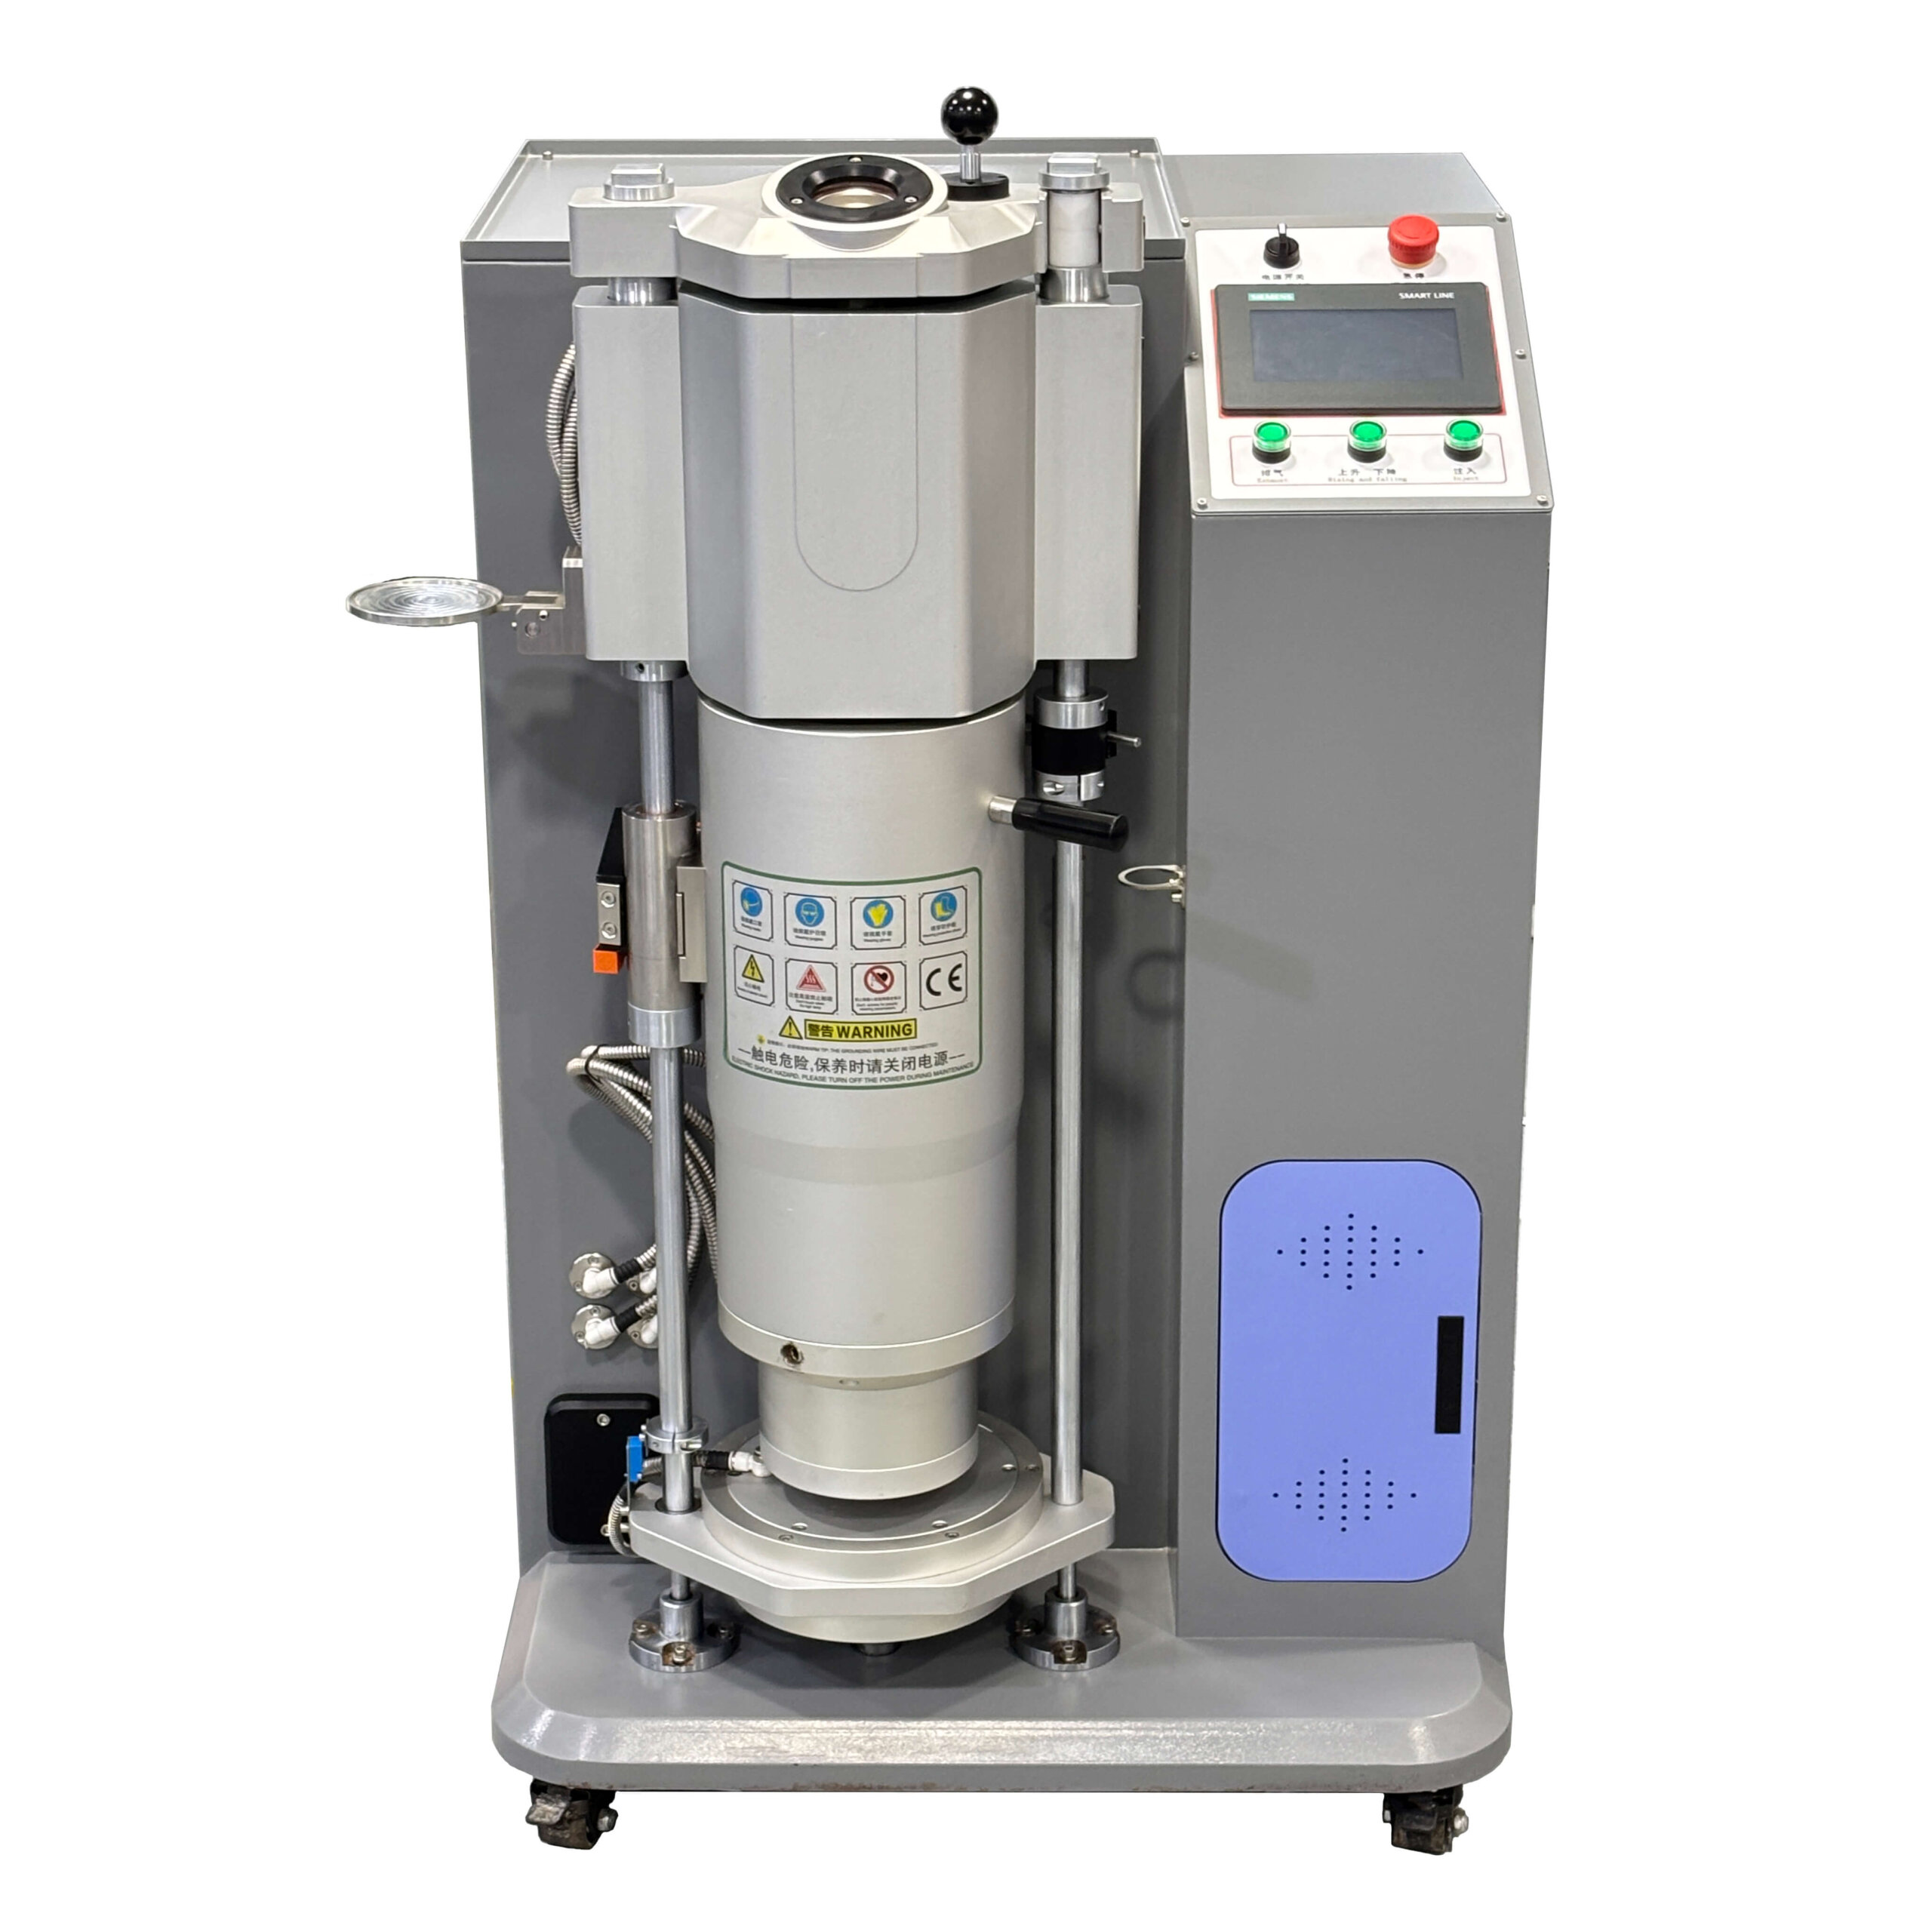
automatic vacuum pressure jewelry casting equipment with sealed aluminum casting chamber

What Is Jewelry Casting Equipment?

Jewelry casting equipment converts a wax or printed pattern into a metal jewelry component through investment casting. The pattern is surrounded by investment material in a flask, removed during burnout, and replaced by molten metal using vacuum, pressure, centrifugal force or a combination of these forces.

The casting machine is the central metal-filling system, but casting quality also depends on wax consistency, investment mixing, burnout completeness, alloy preparation, flask temperature, casting temperature and finishing practice. A buyer should therefore specify the process as one connected line.

Not every “casting machine” serves the same output: flask casting produces jewelry shapes; a continuous casting machine produces wire, rod, strip or bar feedstock; a gold bar casting machine produces bullion. Select from the required final form.

Vacuum Pressure vs Centrifugal Jewelry Casting

The most important decision is how the molten alloy will be driven into the investment mold.

Decision factorVacuum pressure castingVacuum centrifugal casting
Typical metalsGold, karat gold, silver, copper and compatible lower-temperature jewelry alloysPlatinum, palladium, stainless steel and compatible high-temperature alloys
Casting forceVacuum assists air removal; controlled gas pressure drives molten metal through the flaskA rotating arm produces centrifugal force while vacuum and protective atmosphere support the casting cycle
Melting systemInduction melting system commonly designed around graphite crucibles and up to the specified gold/silver alloy rangeHigh-temperature induction system with crucible and temperature measurement selected for platinum-class alloys
Production fitGeneral jewelry factories, goldsmiths, silver jewelry plants and detailed lost wax productionPlatinum workshops, dental or precision high-temperature casting and specialized alloy production
Key buyer checksPressure level, vacuum performance, flask size, gold/silver capacity and automationMaximum working temperature, balance, rotation control, crucible, flask capacity and infrared measurement

Jewelry Casting Equipment Configurations

Compare the workflow and metal requirement before comparing purchase price or automation level.

semi automatic vacuum pressure jewelry casting equipment with separate melting furnace
Separate melting and casting

Semi-Automatic Vacuum Pressure Casting Machine

A separate induction melting furnace supplies molten metal to one or more vacuum pressure casting chambers. This configuration can suit experienced operators and repeated silver or copper-alloy production, but pouring consistency and timing depend more heavily on the operator.

separate meltermanual transferproduction flexibility
automatic vacuum pressure jewelry casting machine for gold silver and copper alloys
Integrated gold and silver casting

Automatic Vacuum Pressure Jewelry Casting Machine

The melting and casting functions are integrated into one controlled cycle. PLC operation can coordinate melting, vacuum, protective gas, pressure and exhaust for repeatable production. Select the model from actual casting weight, flask size, required pressure and daily output.

1–4 kg gold classPLC controlvacuum and pressure
vacuum centrifugal jewelry casting equipment for platinum palladium and stainless steel
High-temperature jewelry alloys

Vacuum Centrifugal Casting Machine

This system melts a smaller high-temperature batch and uses centrifugal force to fill the flask rapidly. It is designed for platinum, palladium, stainless steel and other compatible alloys that require a different temperature, crucible and casting-force strategy from conventional gold and silver pressure casting.

platinumpalladiumcentrifugal force

Equipment Required for a Lost Wax Jewelry Casting Line

Line capacity should be balanced by flasks per cycle and batches per shift so one stage does not become the bottleneck.

01Master and Rubber MoldCreate the master pattern and a repeatable silicone or rubber mold for wax production.
02Wax Injection MachineControl wax temperature, pressure and vacuum to reproduce the required jewelry detail.
03Wax Tree AssemblyAttach patterns to the sprue with appropriate gates, spacing and feed paths.
04Vacuum Gypsum MixerMix investment under vacuum and fill the flask while limiting trapped air.
05Wax Burnout OvenFollow the investment supplier’s ramp, hold and flask-temperature schedule.
06Casting MachineMelt the alloy and fill the prepared flask by pressure or centrifugal force.
07Cooling and DevestingCool or quench according to the alloy and investment before removing the casting tree.
08Cutting and PolishingRemove sprues, deburr, mass-finish, hand-polish, clean and inspect each jewelry component.

Jewelry Finishing and Polishing Equipment

A casting tree is only a semi-finished product. The polishing route must match the alloy, geometry, surface target and amount of material that can safely be removed.

1. Devesting and Plaster Cleaning

Remove the investment according to the alloy’s cooling or quenching procedure, then use suitable water-jet or plaster-cleaning equipment to clear residue from recesses. Check that thin prongs and delicate sections are fully supported during cleaning.

2. Sprue Cutting and Separation

Cut each casting from the tree while leaving enough material for controlled grinding. Select cutters, saws or powered cutting equipment from sprue diameter and production volume, and collect precious-metal offcuts for remelting.

3. Grinding and Deburring

Level the sprue mark, remove flash and correct accessible surface defects with progressively finer abrasives. Aggressive grinding can change dimensions, soften edges or damage stone-setting features, so establish limits for each design.

4. Magnetic Pin Polishing

A magnetic polishing machine drives fine stainless-steel pins around non-magnetic gold, silver and copper-alloy parts. It is useful for burr removal and cleaning around holes, links, prongs and recessed details that are difficult to reach manually.

5. Mass Finishing Machine Selection

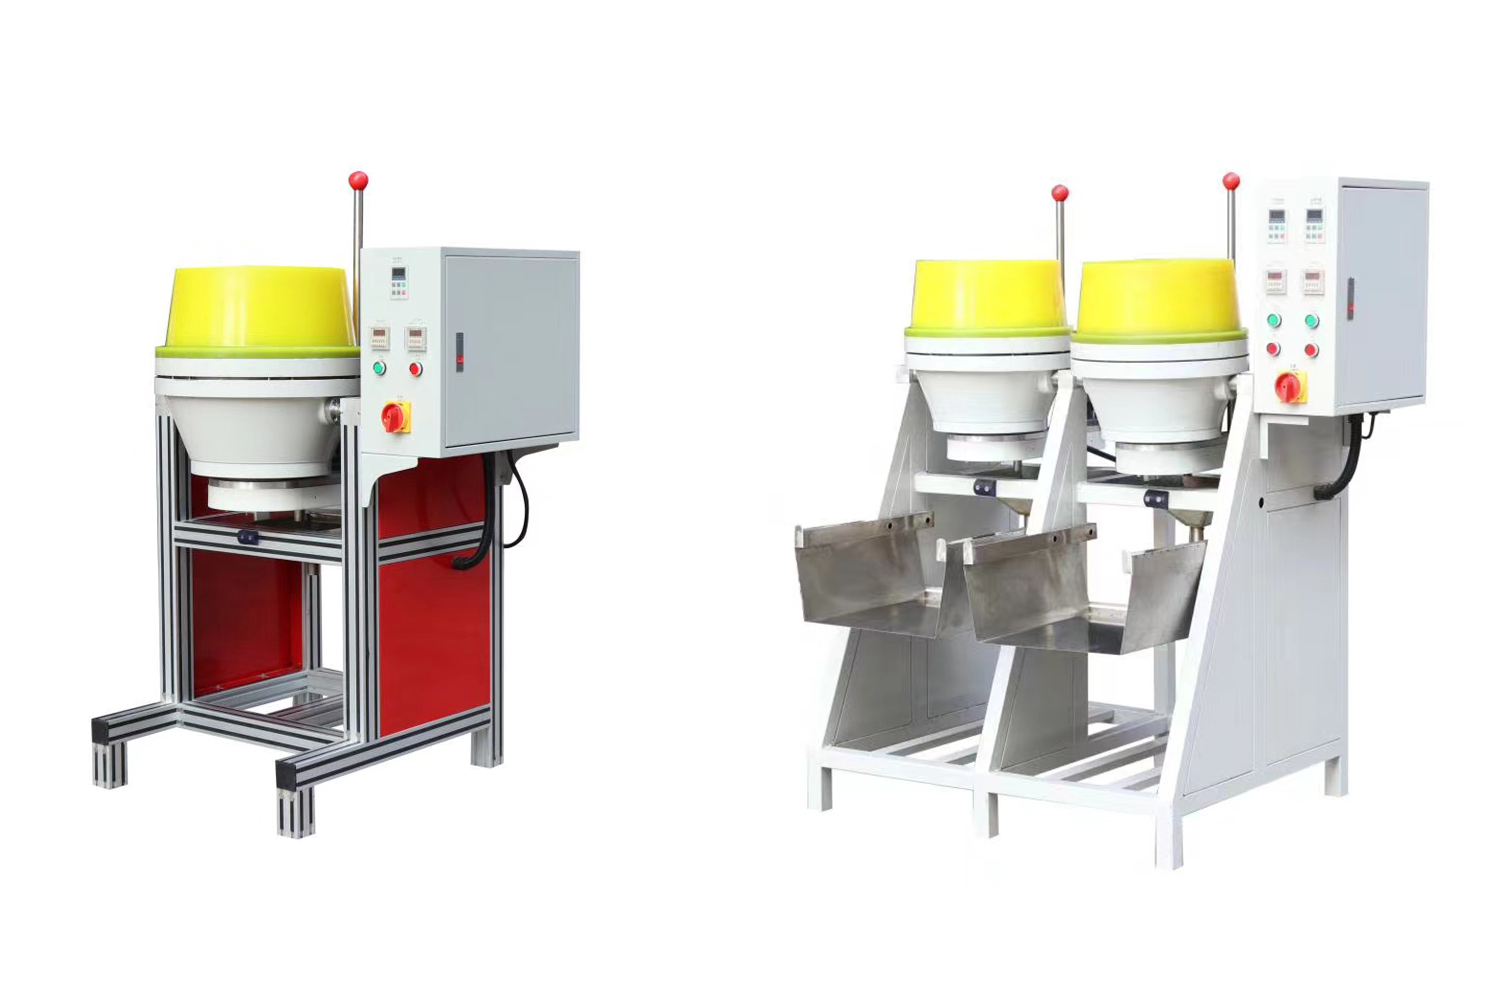
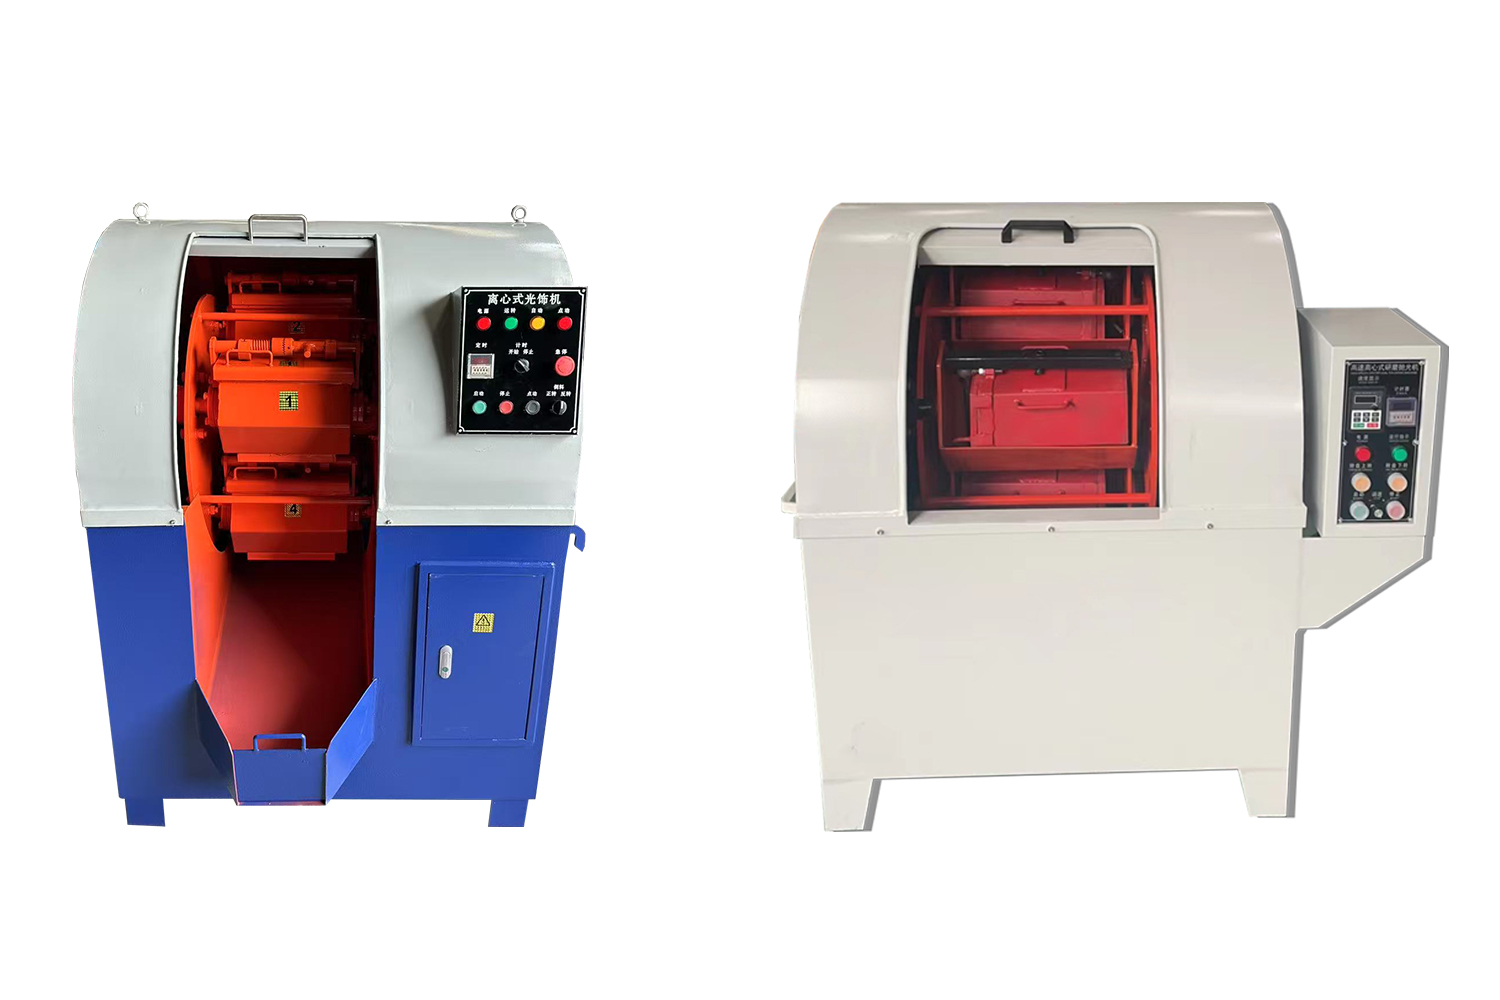
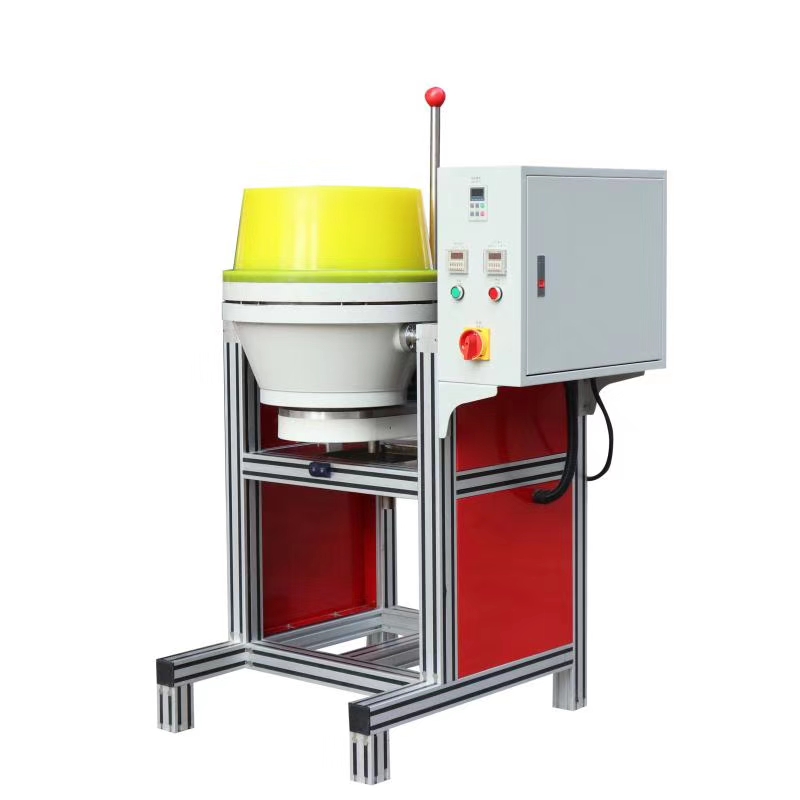
Vibration polishing suits mixed batches and complex surfaces; centrifugal polishing provides faster intensive finishing for small precision parts; wet or dry eddy-current systems can be selected for curved or scratch-sensitive work. Media, compound, speed and cycle time must be tested with the real alloy.

6. Final Buffing, Cleaning and Inspection

Complete the required satin or mirror finish with appropriate compounds and buffing tools, then clean residues ultrasonically or with the approved washing process. Inspect surface, dimensions, sharp details, porosity and stone-setting areas before release.

Plan polishing as part of the casting line: separate media and compounds when alloy contamination matters, control material removal on lightweight jewelry, and recover precious-metal dust, sludge, sprues and rejected parts. Compare CDOCAST jewelry polishing machines for vibration, centrifugal and wet/dry eddy-current finishing.

Vacuum Gypsum Mixer and Burnout Capacity

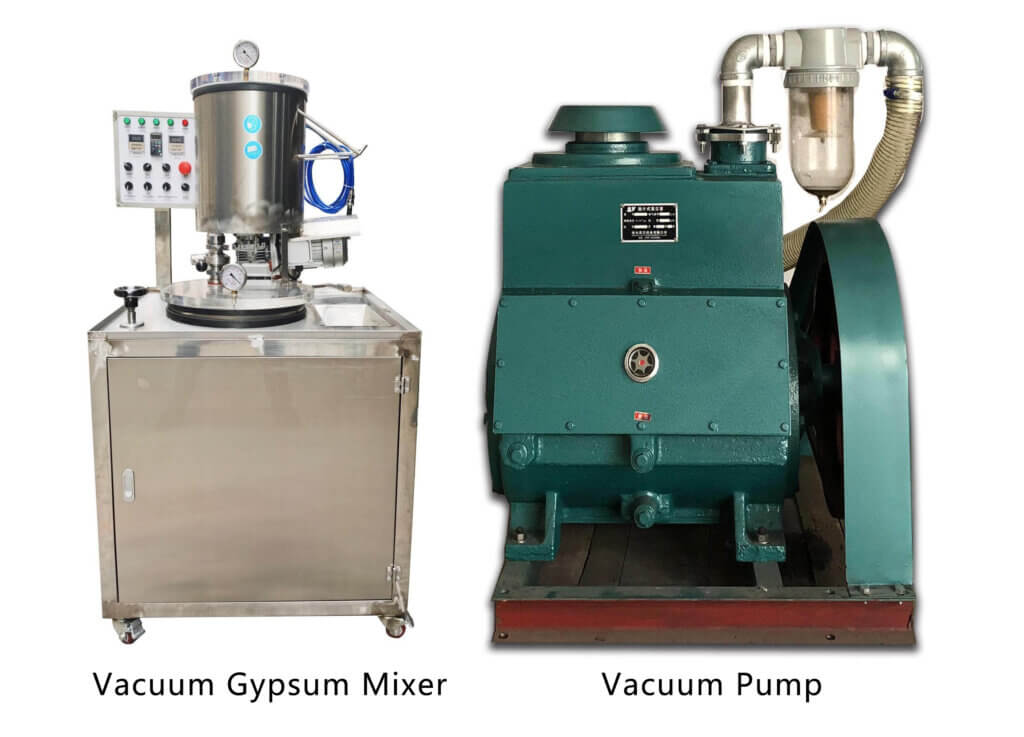
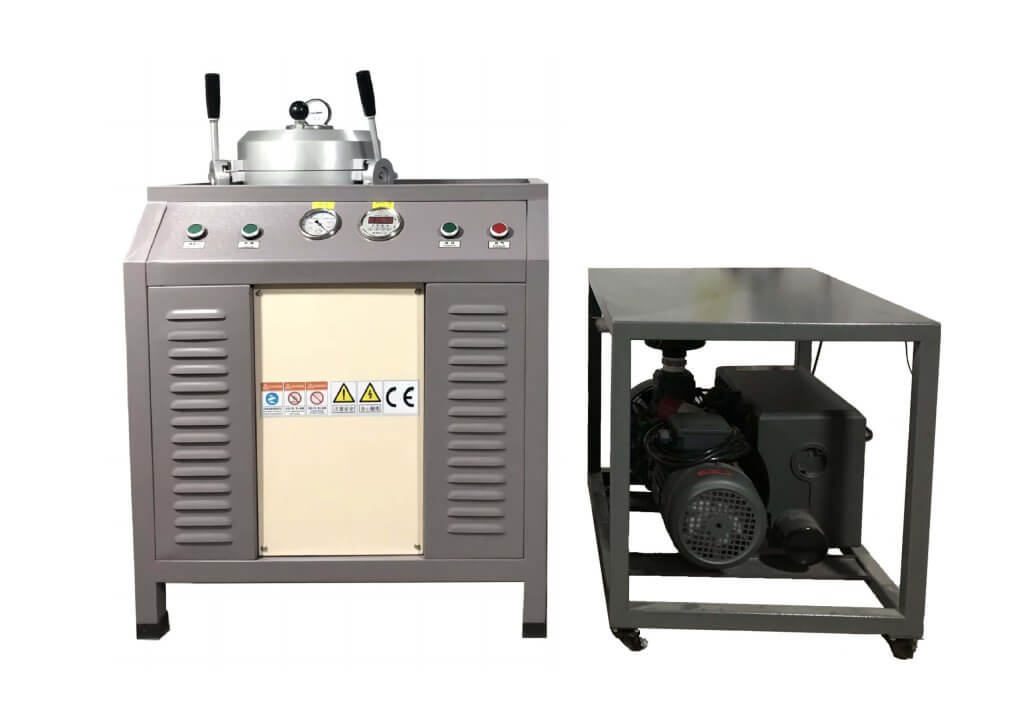
A vacuum gypsum mixer is supporting equipment for investment preparation. Its mixing vessel, lower vacuum chamber, pump and flask capacity should match the number of flasks required by the casting machine and burnout oven.

The burnout oven must hold the intended flask diameter and height with enough spacing for heat circulation. Program capability, temperature uniformity, exhaust arrangement and usable flask quantity are more important than chamber volume alone.

For detailed operating steps, use CDOCAST’s lost wax casting line guide and casting equipment operation guide.

vacuum gypsum mixer and vacuum pump for lost wax jewelry investment casting

Common Casting Problems and Equipment Variables

Defects usually result from interacting pattern, investment, burnout, alloy and machine conditions.

Observed problemVariables to investigatePurchasing implication
Incomplete fine detailsMetal and flask temperature, pressure or centrifugal force, sprue design, alloy fluidity and investment permeabilityTest the thinnest real design at the required flask size before acceptance
Gas porosityWax residue, investment mixing, burnout, melt atmosphere, alloy cleanliness and vacuum integritySpecify vacuum performance, protective gas and repeatable burnout control
Shrinkage porositySprue feeding, reservoir design, section thickness, cooling sequence and casting parametersMachine pressure cannot replace correct jewelry feeding and pattern design
Rough or reacted surfaceInvestment compatibility, excessive temperature, incomplete burnout, alloy reaction and atmosphereConfirm investment and crucible compatibility with the actual metal
Cracked investmentMix ratio, vacuum time, handling, burnout ramp, flask preparation and thermal shockInclude mixer consistency and programmable burnout control in line planning

Jewelry Casting Equipment Purchase Checklist

Send these details before requesting a final machine configuration or casting test.

Metals, karats and complete alloy compositions to be cast
Normal casting weight, maximum casting weight and batches per shift
Smallest feature, thinnest section and most difficult jewelry design
Flask diameter, height, quantity per cycle and required burnout capacity
Vacuum pressure or centrifugal casting method required by the alloy
Manual, semi-automatic or PLC-controlled operating preference
Available voltage, compressed air, protective gas and cooling water
Wax injector, mixer, vacuum pump, burnout oven and finishing equipment
Consumables: crucibles, flasks, investment, seals and temperature sensors
Acceptance test using the customer’s alloy, flask and difficult jewelry pattern
Safety planning: molten metal, hot flasks, investment dust, burnout exhaust, compressed gas and rotating equipment require site-specific risk assessment, ventilation, guarding, dry tools, suitable PPE and trained operators. Review applicable local requirements and authoritative molten-metal safety guidance before commissioning.

Related Jewelry Casting Resources

These pages separate product specifications, model selection and operating instructions.

Jewelry Casting Equipment FAQ

Answers to the questions buyers should settle before choosing the casting method and line capacity.

What equipment is needed for lost wax jewelry casting?

A practical line normally includes master-pattern and rubber-mold tools, a wax injector, wax-tree tools, vacuum investment mixing equipment, flasks, a burnout oven, the selected jewelry casting machine, cooling or devesting equipment, sprue cutting, grinding, cleaning and polishing equipment.

Should I choose vacuum pressure or centrifugal jewelry casting equipment?

Vacuum pressure casting is generally selected for gold, karat gold, silver and compatible copper alloys. Vacuum centrifugal casting is selected for platinum, palladium, stainless steel and compatible high-temperature alloys. Confirm the actual alloy and design with a casting test.

Can one jewelry casting machine cast gold, silver and platinum?

A gold and silver pressure casting machine is not automatically suitable for platinum. Platinum requires a much higher-temperature melting system, compatible crucible, suitable temperature measurement and an appropriate casting-force method. A dedicated centrifugal platinum casting configuration is normally recommended.

How should jewelry casting machine capacity be selected?

Use the true metal weight of one casting tree, the number of trees per shift, flask size and cycle time. Capacity must be confirmed separately for gold, silver and other alloys because metal density changes the weight held by the same crucible volume.

Why is a vacuum gypsum mixer important?

Mixing investment under vacuum helps limit trapped air before the flask is filled. It does not correct an unsuitable powder-to-water ratio or poor working time, so the mixer, vacuum pump and operator procedure must follow the investment supplier’s process.

Does automatic jewelry casting eliminate casting defects?

No. Automation improves repeatability of melting, vacuum, pressure and timing, but wax quality, sprue design, investment mixing, burnout, alloy cleanliness and flask temperature still determine the final result.

What should a jewelry casting equipment acceptance test include?

Use the customer’s alloy, intended flask, normal casting weight and a design containing the smallest feature and thinnest section expected in production. Record cycle settings, temperatures, vacuum or pressure behavior, filling completeness, porosity, surface condition and repeatability over multiple casts.

Configure the Casting Method and Complete Line

Send the alloy, casting-tree weight, flask size, daily output and most difficult jewelry design. CDOCAST can match the casting machine, investment equipment, burnout capacity and acceptance test to the production target.

Discuss Your Jewelry Casting Line