Logo and Character Stamping Dies
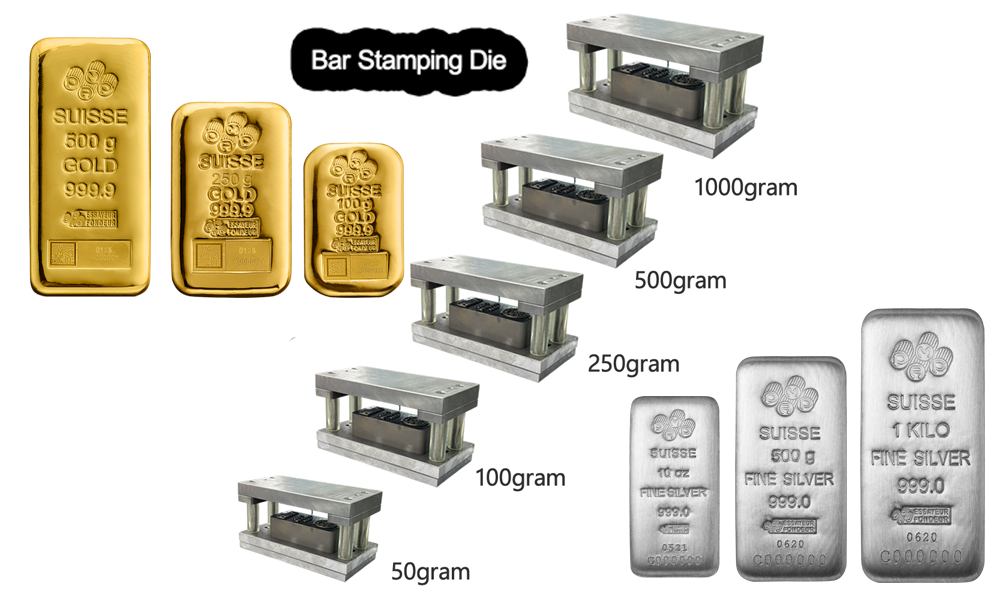
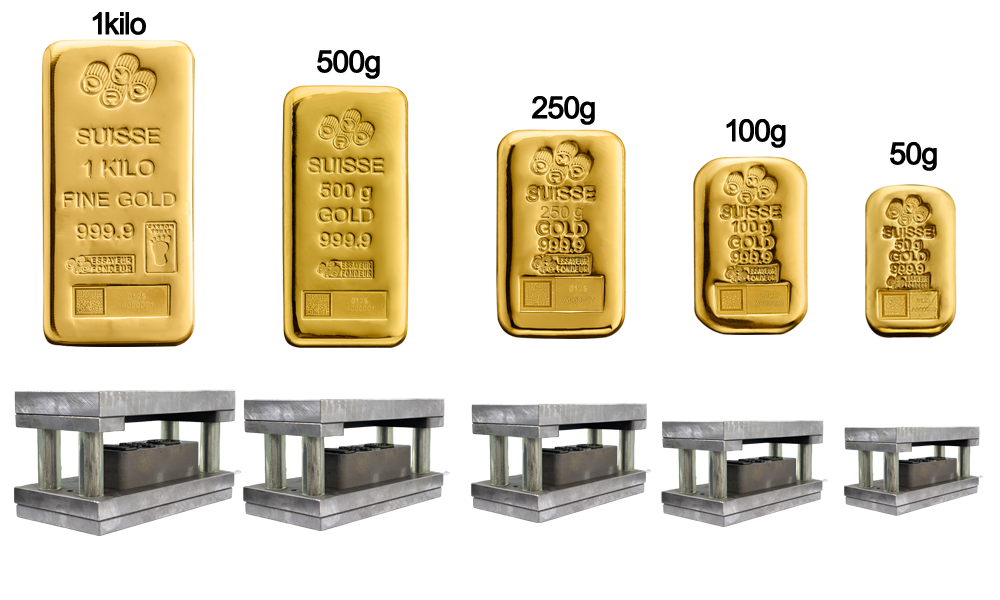
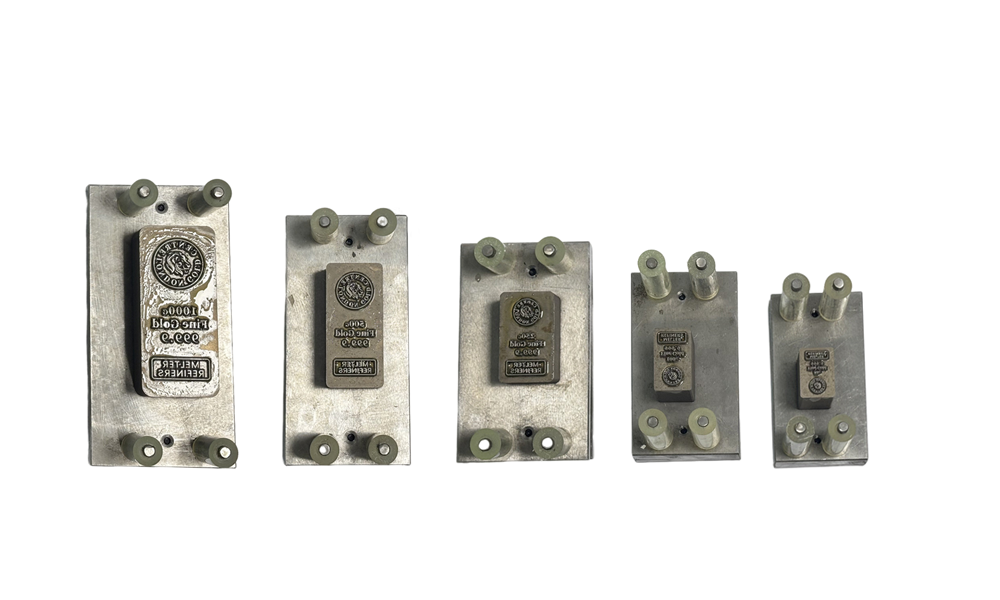
Used for stamping logos, purity marks, serial numbers, weight information, and brand characters on gold bars, silver bars, and bullion products.
 cdocast
Customized The Die For Gold Silver Minting & Casting Bar
Custom Minting Tooling
CDOCAST designs and manufactures precision coin minting dies, gold and silver bar stamping dies, serial number die systems, logo dies, character dies, casting dies, blanking tools, and quick-change tooling for mints, refineries, bullion producers, and precious metal workshops.

Different precious metal products require different die structures. The right tooling depends on product shape, metal type, press compatibility, artwork depth, surface finish, and expected production volume.
Used for stamping logos, purity marks, serial numbers, weight information, and brand characters on gold bars, silver bars, and bullion products.
Designed for high-detail coins, medals, commemorative products, and proof-style surfaces requiring sharp relief, clean edges, and stable repeatability.
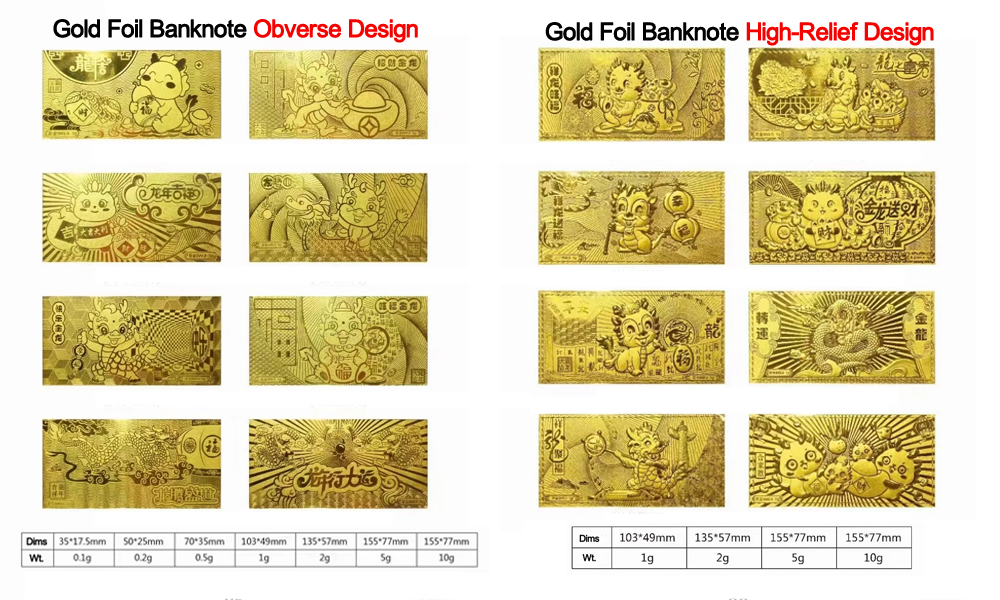
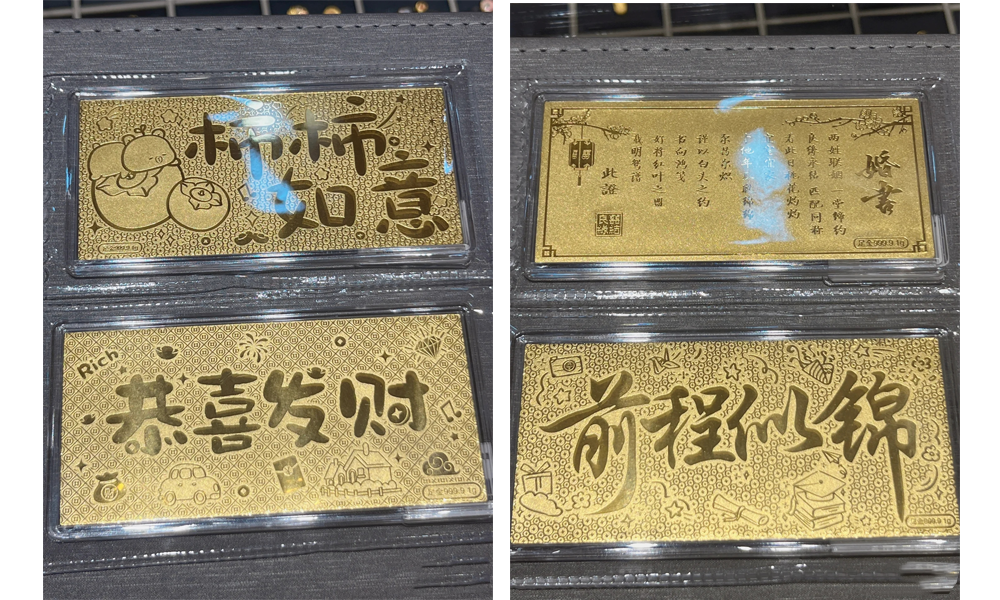
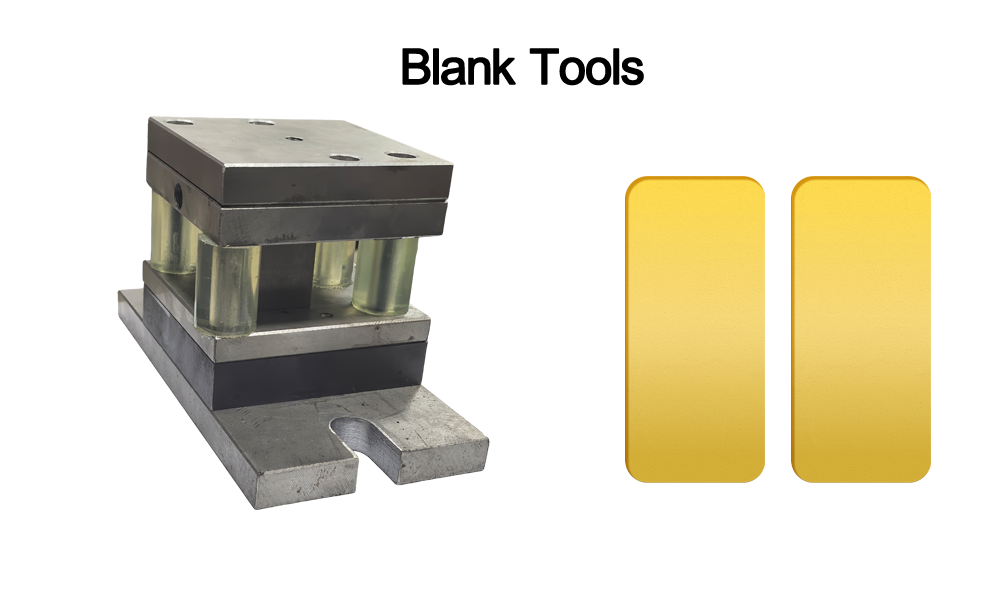
Custom tooling for bar casting shapes, gold foil banknotes, blanks, and supporting processes before final minting, stamping, or packaging.
These examples show common CDOCAST tooling options for serial number dies, coin minting dies, bar stamping dies, custom logo stamping dies, blank tooling, and gold foil banknote dies.


A die is not only a piece of steel. It directly affects product appearance, press stability, die life, operator safety, and whether each coin or bar keeps the same premium finish.
| Feature | CDOCAST Approach | Production Benefit |
|---|---|---|
| Precision detail | CNC machining and EDM processing for fine relief, sharp text, and complex patterns | Cleaner logos, clearer characters, and stronger brand presentation on coins and bars. |
| Tool steel selection | Durable die steel options such as DC53 according to product and press requirements | Better wear resistance and longer die life under repeated minting or stamping pressure. |
| Surface finish | Mirror, satin, relief, and dual-surface finishing options | Supports premium coin surfaces, clean bullion marks, and different visual styles. |
| Quick-change tooling | Die structures designed for safer and more efficient installation on compatible presses | Reduces downtime when switching logos, product sizes, or production batches. |
| Serial number marking | Custom serial number die layouts for numbered gold bars, silver bars, and traceable bullion products | Helps refineries and bullion brands add product identification, batch control, and anti-counterfeit marking. |
| Process support | Die design matched with press tonnage, metal hardness, product thickness, and artwork depth | Helps avoid shallow marks, die damage, misalignment, and unstable stamping results. |
CDOCAST die production follows a controlled workflow from artwork review to blank preparation, machining, finishing, and final inspection.
Proper care helps protect the mirror surface, reduce rust risk, prevent accidental scratches, and extend the working life of coin minting dies and bar stamping dies.
Keep the die surface separated, cushioned, and protected from impact during packing, shipping, and workshop handling.
Apply suitable anti-rust oil or protective coating when dies are stored, especially in humid workshops or long storage periods.
Inspect alignment, surface cleanliness, press setup, and product blank condition before each production batch.
Avoid touching polished die surfaces with hard tools or dirty gloves, as small scratches can appear on finished coins or bars.
Keep dies away from corrosive chemicals, moisture, dust, and uncontrolled temperature changes.
Use the correct press tonnage and installation structure to avoid uneven pressure, misalignment, or premature die damage.
Custom dies work best when they are matched with the right press, stamping system, punching machine, and bullion production process.
 Hydraulic Press for Minting Hydraulic coin minting press for gold coins, silver coins, medals, and bullion bar stamping with matched custom dies.
 Hydraulic Logo Stamping Machine Logo stamping equipment for accurate brand marks, purity marks, weight marks, and serial details.
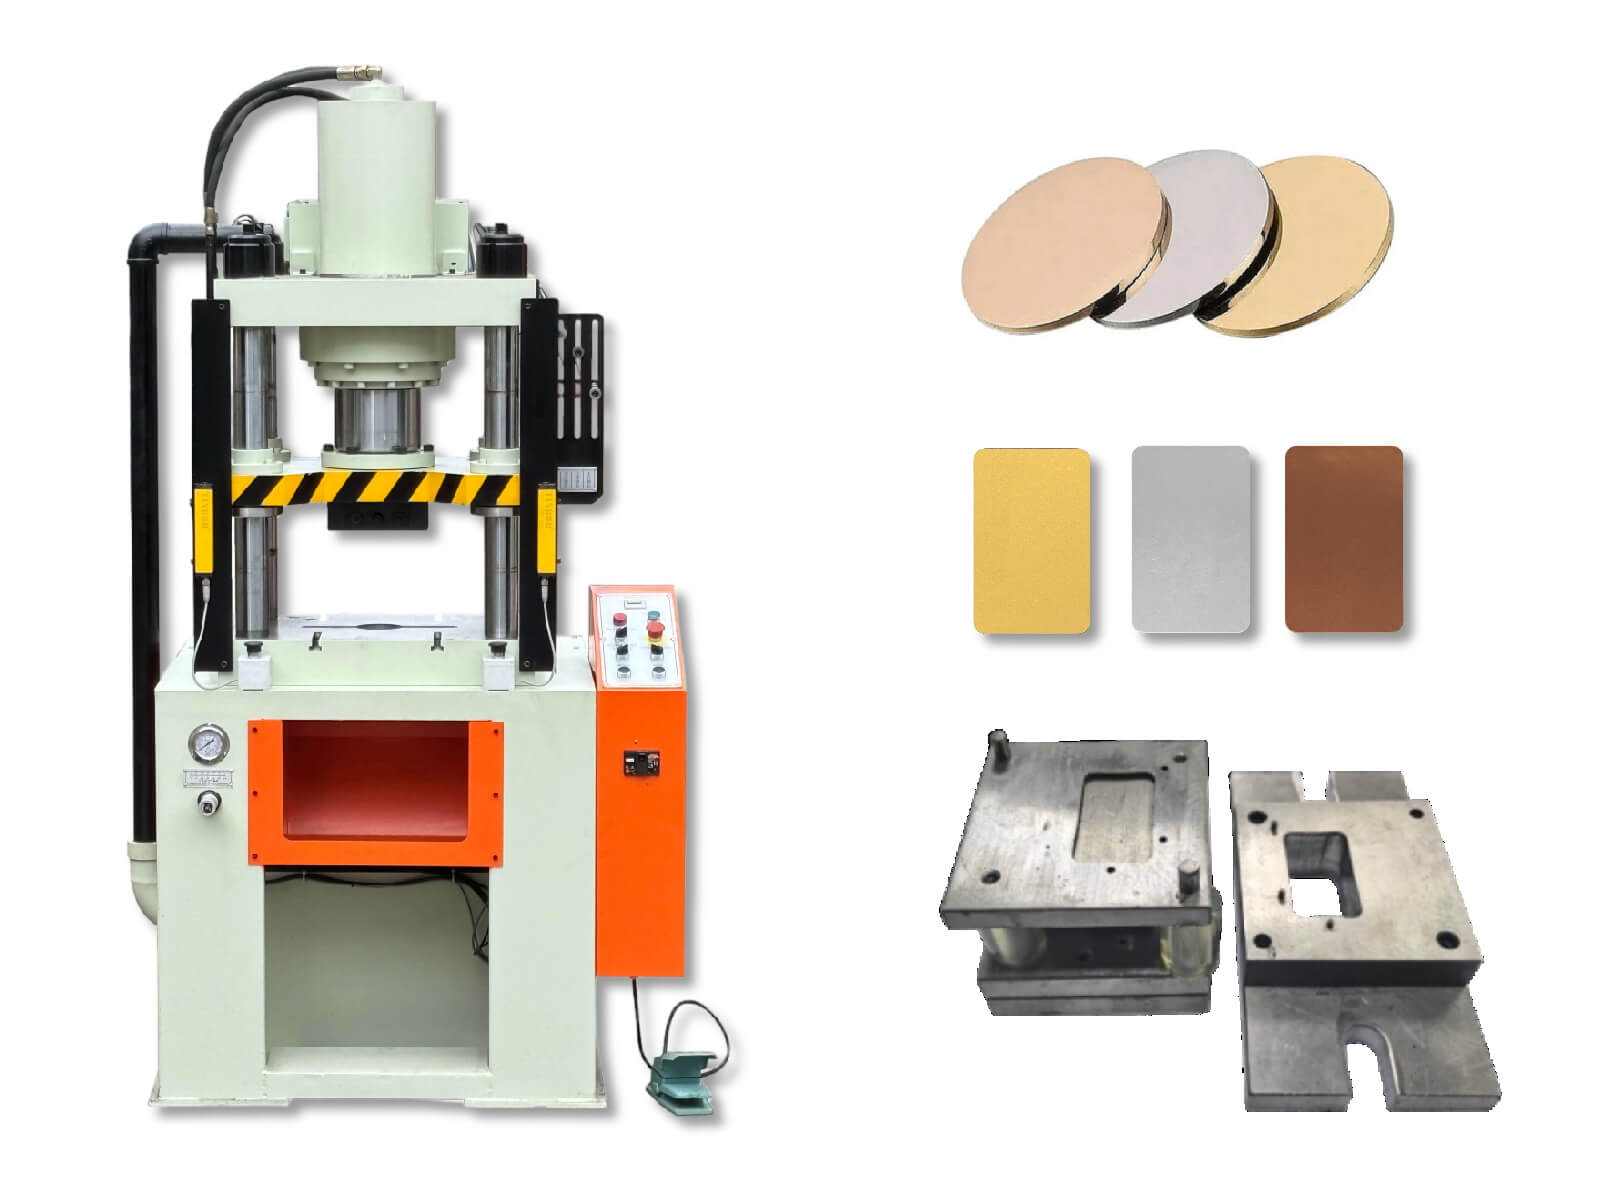 Hydraulic Punching Machine Punching equipment for preparing blanks and supporting coin, medal, and precious metal sheet production.
These questions help buyers compare die material, cutting process, die holder design, service life, delivery time, and stamping accuracy before ordering custom tooling.
CDOCAST dies use imported heat-treated tool steel materials and slow wire cutting for accurate edges and stable details. Low-cost dies may use simpler hand-cutting or less controlled processing, which can affect precision, die life, and stamping consistency.
Our die holders are made with a black oxide heat treatment process to improve rust resistance during long sea transportation and workshop storage. The final service life depends on press tonnage, metal hardness, stamping depth, alignment, and daily maintenance.
CDOCAST logo stamping dies are supplied with a die holder and positioning groove. The groove is designed according to the gold bar or silver bar size, so the customer can place the bar directly into the slot and press an accurate logo or pattern without manual positioning.
We can provide free design support, customized die holder design, slow wire cutting, imported heat-treated steel materials, positioning slots for accurate stamping, and fast delivery. For many standard logo stamping die projects, delivery can be arranged in about 7 days after artwork confirmation.
Please provide product size, coin or bar thickness, artwork file, logo position, relief depth, metal type, surface finish, press model, and expected production volume. For bar stamping dies, the exact gold bar or silver bar dimensions are important for designing the positioning groove.
Yes. CDOCAST can design serial number die systems for numbered bullion bars, refinery batch marks, product traceability, and anti-counterfeit marking. Buyers should confirm the bar size, marking area, number format, press model, and whether the serial number design needs fixed or changeable numbering.
It depends on product size, metal hardness, press tonnage, and required marking depth. In many cases, separate die settings or dedicated dies provide better repeatability and more stable surface quality.
Use the correct press tonnage, keep the die surface clean, avoid moisture and corrosive chemicals, protect mirror areas, apply anti-rust treatment during storage, and inspect alignment before production.
Send your artwork, product size, metal type, press model, and surface finish requirement. CDOCAST can recommend a suitable die structure and provide a custom quotation.
During transportation, pay special attention to protecting the delicate custom coin dies surface, as engraved graphics are highly susceptible to micro-scratches.
When high-capacity gold bar minting dies are not in use, always apply anti-rust oil. Before placing them back into the hydraulic press, ensure all oil residue is thoroughly wiped off.
Before launching a bullion strike, thoroughly inspect both raw material planchets and the hydraulic coining press dies surface to ensure they are free of dust, micro-debris, or metal contaminants.
For industrial silver bar minting dies featuring proof-like mirror backgrounds, perform regular maintenance polishing using a fine wool buffing wheel and specialized polishing compounds.
Store your precision coin press dies in a strictly controlled room (stable temperature/low humidity) to prevent micro thermal deformation and chemical corrosion from acidic exposure.
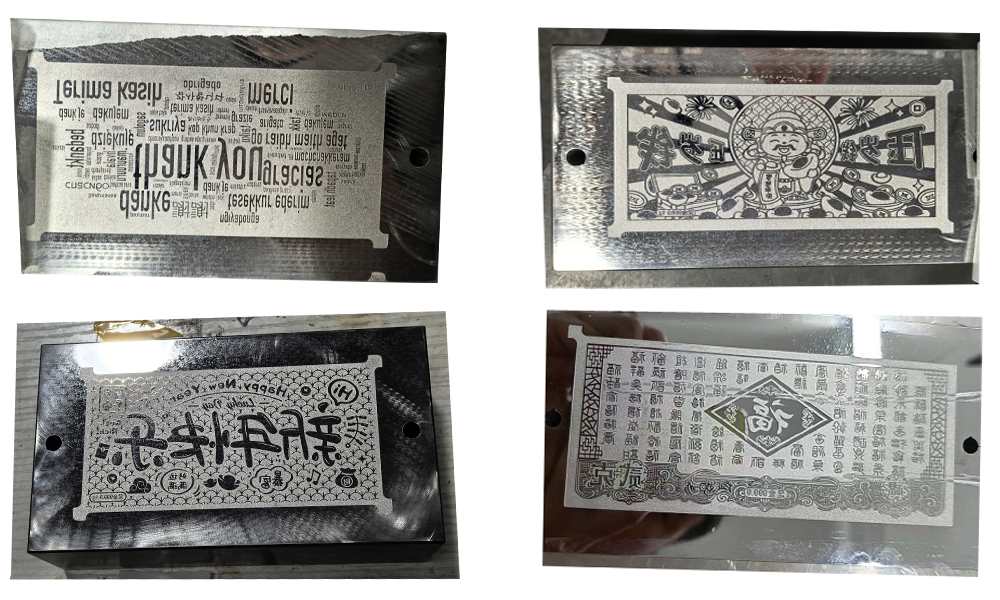
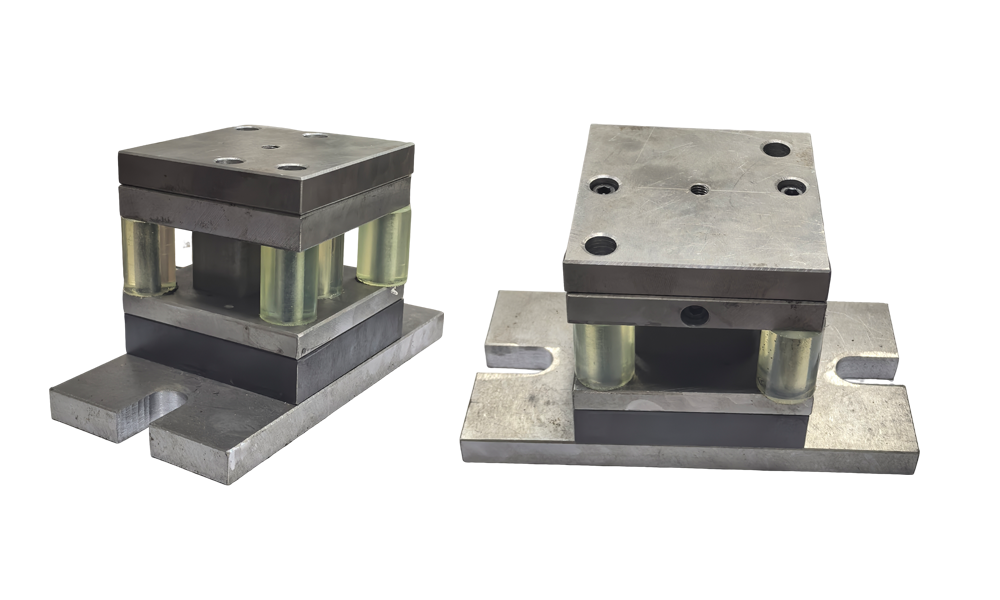
Die Making:
The artistic designs on mint coins and medals aren’t etched into each coin – they’re pressed. To press a design onto coins and medals, the Mint needs a stamp called a die. To make a die, the Mint uses another stamp called a hub.
Once the customer approves a design, our engineer turns the line drawing into a sculpted piece of art using digital software. A machine engraves the design onto a copper hub, which shows the positive image the way the artist created it. Dies are like a photo negative, displaying the design in reverse. When the dies stamp the coins or medals, the positive image transfers onto the blank.
To create dies, a wire EDM machine first cuts the steel block into cylindrical sections (3-inch diameter). These cylinders then undergo three-stage heat treatment to achieve the required hardness and stability. Only after this process can the actual die machining begin.
The heat-treated cylinder is further shaped, with one end precision-ground into a cone and polished to a smooth, shiny surface. This cone-shaped workpiece is referred to as a die blank.
The uses DC53 steel for dies because it is strong enough to withstand being forced against other metals in the coin press.
A CNC milling machine precisely engraves the design onto the reusable copper hub. This component serves as a master mold for reproducing the desired pattern and can be reused for multiple production cycles.
After EDM processing, the dies undergo manual polishing to achieve the required surface finish—whether a mirror polish or textured (satin) finish per customer specifications.
A technician then cleans and inspects each die under a microscope, removing minor scratches or imperfections through precision buffing.
Total Lead Time: 7–10 days for the complete die manufacturing process.