Confirm outside diameter, wall thickness, seam condition, straightness and whether the material requires annealing.
 cdocast
- Call Us: 008615168765707
- Mail Us: sales@cdocast.com
cdocastBuy the Most advanced Tube Necking Machine
CDOCAST CDO-TN1 reduces and tapers the end of Φ2–12 mm precious-metal tube. The formed lead end can enter a tube drawing die more easily, helping prepare gold, silver, copper and compatible alloy tubes for subsequent reduction and sizing.

A tube necking machine forms a reduced or tapered section at the end of a metal tube. For precious-metal tube production, this smaller lead end is especially useful before tube drawing: it gives the operator a section that can pass through the drawing die and be gripped for the next reduction.
The CDO-TN1 is a tube-end forming machine for gold, silver, copper and suitable alloy tube. With matching dies, it can serve as a gold tube necking machine, silver tube necking machine or copper tube end reducer. It uses a motor-driven forming head, a 100 mm D2 tool and an electric lubrication system. It does not replace a tube drawing machine; it prepares the tube end for drawing or another downstream operation.

One compact model covers the published Φ2–12 mm working range with customized tooling selected from the tube specification.

Designed to prepare tapered tube ends for drawing, sizing or other downstream operations without cutting away the tube end.
The table follows the CDOCAST tube-forming catalog and the published CDO-TN1 product specification.
| Specification | CDO-TN1 |
|---|---|
| Voltage | 380 V, 3 phase, 50 Hz |
| Motor power | 3 kW |
| Maximum tube diameter | Φ12 mm |
| Minimum tube diameter | Φ2 mm |
| Maximum necking ratio | ≤50% |
| Die material and hardness | D2, HRC 60–62 |
| Die length | 100 mm |
| Lubrication system | Three-phase electric pump |
| Machine size (L×W×H) | 730×480×1050 mm |
| Machine weight | 350 kg |
Correct tooling and lubrication are essential when reducing thin-wall gold, silver or copper tube.
Confirm outside diameter, wall thickness, seam condition, straightness and whether the material requires annealing.
Match the D2 necking tool to the incoming tube and required lead-end diameter, length and taper.
Insert the specified length into the forming head and reduce the end progressively without exceeding the approved reduction.
Check the neck diameter, taper length, concentricity and surface before feeding the tube into the drawing die.
The compact layout keeps the working head, controls and lubrication connection accessible to the operator.

Final die selection should follow the actual alloy, wall thickness and drawing schedule rather than material name alone.
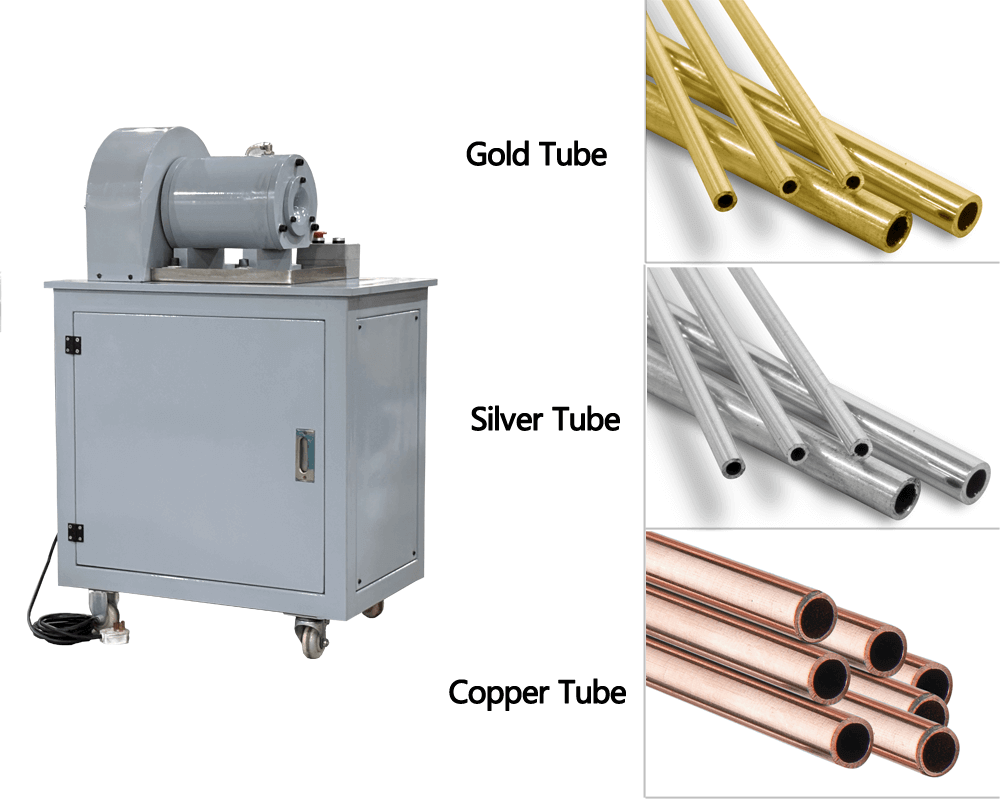
Supports tube-end preparation for gold, K-gold, silver, copper and compatible alloys within the specified diameter range.

Creates a reduced tube end that can enter a smaller drawing die and provide a gripping section for downstream reduction.
Send both incoming and required neck dimensions so the tooling can be evaluated correctly.
Necking is normally positioned between initial tube forming and subsequent tube drawing or annealing.
Review the tube-forming series, then send the incoming tube and required neck dimensions for tooling selection.
Purchasing answers for jewelry and precious-metal tube manufacturers.
It reduces or tapers the tube end. In precious-metal tube production, the smaller lead end helps the tube enter a drawing die and gives the operator a section that can be gripped for the next reduction.
The published specification lists a working range from Φ2 mm to Φ12 mm. Tooling must still be matched to the exact outside diameter, wall thickness and required neck profile.
The catalog lists a maximum necking ratio of ≤50%. The practical reduction for a specific tube depends on alloy ductility, wall thickness, seam condition, annealing state and die geometry.
Yes, these are the primary published applications. Provide the alloy and temper because fine gold, K-gold, silver and copper do not behave identically during tube-end reduction.
No. Necking prepares a reduced section at the tube end. Tube drawing pulls the tube through a die to reduce and size a longer section or the entire tube.
The terms can overlap in some markets, but the required operation should be defined clearly. CDO-TN1 is presented here for tapered tube-end reduction and drawing-die preparation; buyers needing full-length rotary swaging should provide a separate process drawing.
Provide the material, incoming outside diameter and wall thickness, final neck diameter and length, taper profile, tube length, production quantity, downstream drawing-die size and factory voltage.
Send CDOCAST your tube drawing, alloy, wall thickness and required neck profile for CDO-TN1 tooling evaluation.