
12-Roller Configuration
CDO-RM12
For controlled reduction where a 12-roller line and up to 62 m/min published speed match the production target.
InletØ16 / 14 / 12 / 9 mm
OutletØ7 / 6 / 5 / 3.8 mm
Main motor18.5 kW
Weight3 t
 cdocast
The Most Advanced Rolling Mill For Rolling SIzes gold, silver, copperwire
CDOCAST multi-pass wire rolling machines reduce precious-metal and copper wire rod through alternating horizontal and vertical roller stands, providing controlled diameter reduction before final wire drawing.
A metal wire rolling mill is a continuous wire-reduction machine that uses driven rollers instead of drawing dies to progressively reduce the diameter of gold, silver, K-gold, copper and suitable alloy wire rod. Multiple roll boxes are arranged along a straight production path, with horizontal and vertical rolls helping control deformation from pass to pass.
The CDOCAST system combines wire straightening, rolling stands, spray cooling and lubrication, inverter speed control, traction and take-up. Depending on the processed material, it can serve as a gold wire rolling mill, silver wire rolling machine or copper wire rolling machine for efficient intermediate reduction before final drawing, sizing or forming.
Choose the machine from inlet diameter, required outlet range, line speed, material hardness and downstream drawing plan.
For controlled reduction where a 12-roller line and up to 62 m/min published speed match the production target.
For customers requiring a wider staged reduction range and the highest published line speed in this series.
A heavier 37 kW version for demanding material and production requirements, with a larger machine frame.
The comparison below retains the specifications published on the original CDOCAST product page.
| Specification | CDO-RM12 | CDO-RM16 | CDO-RM16B |
|---|---|---|---|
| Inlet wire diameter | Ø16 / Ø14 / Ø12 / Ø9 mm | Ø16 / Ø14 / Ø12 / Ø10.5 mm | Ø12 mm |
| Outlet wire diameter | Ø7 / Ø6 / Ø5 / Ø3.8 mm | Ø5.2 / Ø4.6 / Ø3.8 / Ø3.4 mm | Ø3.8 mm |
| Roller quantity | 12 | 16 | 16 |
| Cooling method | Spray cooling | Spray cooling | Spray cooling |
| Main motor power | 18.5 kW | 18.5 kW | 37 kW |
| Speed control | Inverter control | Inverter control | Inverter control |
| Voltage | 380 V | 380 V | 380 V |
| Water-pump motor | 0.25 kW | 0.25 kW | 0.25 kW |
| Maximum speed | 62 m/min | 85 m/min | 74 m/min |
| Roller compression ratio | 16% | 16% | 16% |
| Machine dimensions | 3300×900×1360 mm | 3850×900×1360 mm | 4945×1100×1700 mm |
| Machine weight | 3 t | 3.5 t | 5.5 t |
The line combines mechanical reduction, cooling, speed control and collection in one continuous path.
Incoming rod is aligned and guided into the first rolling stand for stable entry.
Alternating roll directions reduce the wire progressively and distribute deformation between passes.
Spray cooling helps manage roller and workpiece temperature while supporting stable operation.
The reduced wire exits through the traction system and is collected for annealing, drawing or forming.
Real machine images help buyers evaluate the line layout, roller section and operator access before ordering.

Each roll box contains longitudinal and transverse rolling pairs. Equalized pass design reduces the wire in stages according to material elongation characteristics.
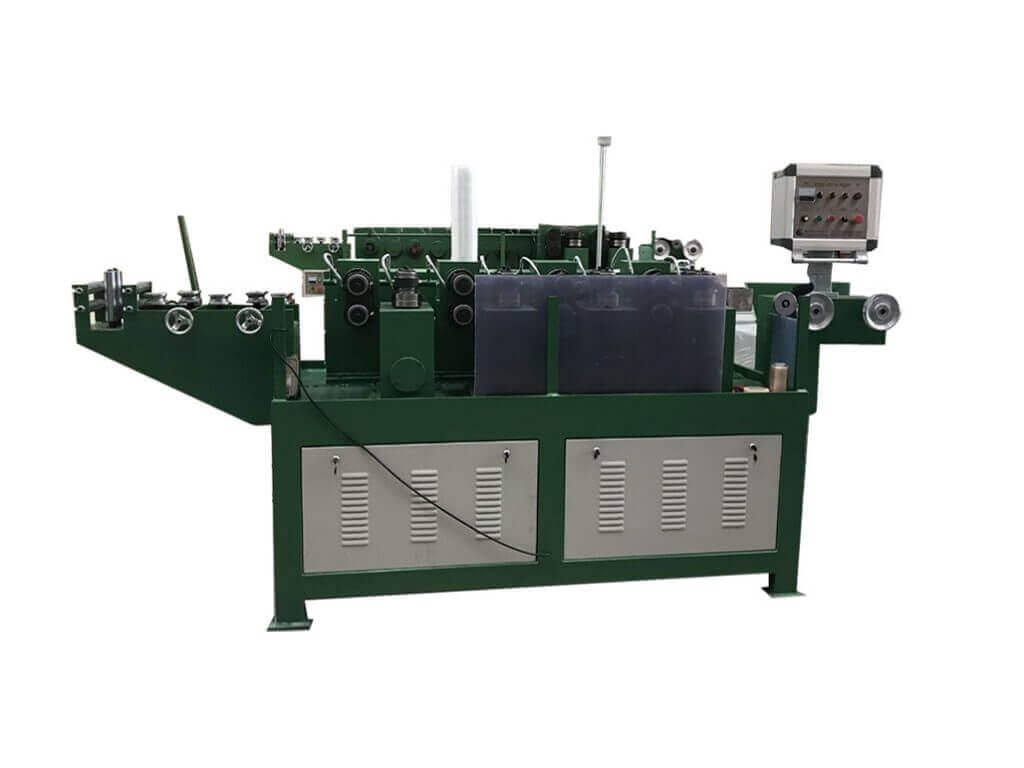
Helical and spiral-bevel gearing, inverter speed control, spray lubrication and traction coordinate wire movement through the rolling line.
The main benefits apply to intermediate wire reduction before final precision drawing.
Roll-based reduction avoids repeated die threading during this intermediate process and can reduce setup labor.
The driven roller configuration provides strong adaptability for materials that may be difficult for a general high-speed mill.
A straight wire path and limited slip through the rollers reduce unnecessary bending, friction and operating noise.
Stepless speed control helps match line speed to material, inlet diameter, reduction plan and cooling condition.
Special alloy-steel rollers receive heat treatment for wear resistance and impact resistance in production.
Progressive rolling can produce a denser structure and reduce wire-break risk during subsequent drawing.
A useful quotation requires the complete route from incoming rod to the final wire specification.
Connect rolling with annealing and final drawing to create a practical wire-production route.
Review the three model specifications, then provide your material, inlet diameter, outlet target and hourly output.
Practical answers for buyers comparing wire rolling and wire drawing equipment.
It is designed for pure silver, silver alloys, pure gold, K-gold, copper, copper alloys and other suitable wire materials within the selected model’s diameter and power range.
Not usually. Roller reduction can leave some ovality. A final wire drawing machine is recommended when the product requires accurate roundness, calibrated diameter and a smoother surface.
CDO-RM16 has the highest published maximum speed at 85 m/min. Actual production speed depends on material, diameter reduction, cooling, take-up and process stability.
The original product guidance recommends using a separate winder for silver, K-gold and similar alloy wire so the processed material can be collected without becoming loose or scattered.
All three published models use spray cooling, with a 0.25 kW water-pump motor. Water quality, filtration, flow and maintenance should be planned for the installed line.
CDO-RM12 uses 12 rollers and has a published maximum speed of 62 m/min. CDO-RM16 uses 16 rollers, provides a different staged diameter range and has a published maximum speed of 85 m/min.
Provide the metal or alloy, hardness, inlet diameter, outlet diameter after rolling, final drawn diameter, hourly output, reel requirement, voltage and available workshop space.
Send CDOCAST your material, inlet diameter, target outlet, hourly output and final wire requirement for a matched rolling, winding, annealing and drawing solution.