CDO-EX250T Metal Extrusion Press
Entry model for smaller approved nonferrous billets and product sections. Its published billet size is Φ40×140 mm.
Thrust250T
BilletΦ40×140 mm
Main motor7.5 kW
Max pressure22 MPa
 cdocast
Buy the Most advanced Metal Extrusion Machine For Types Of Metals
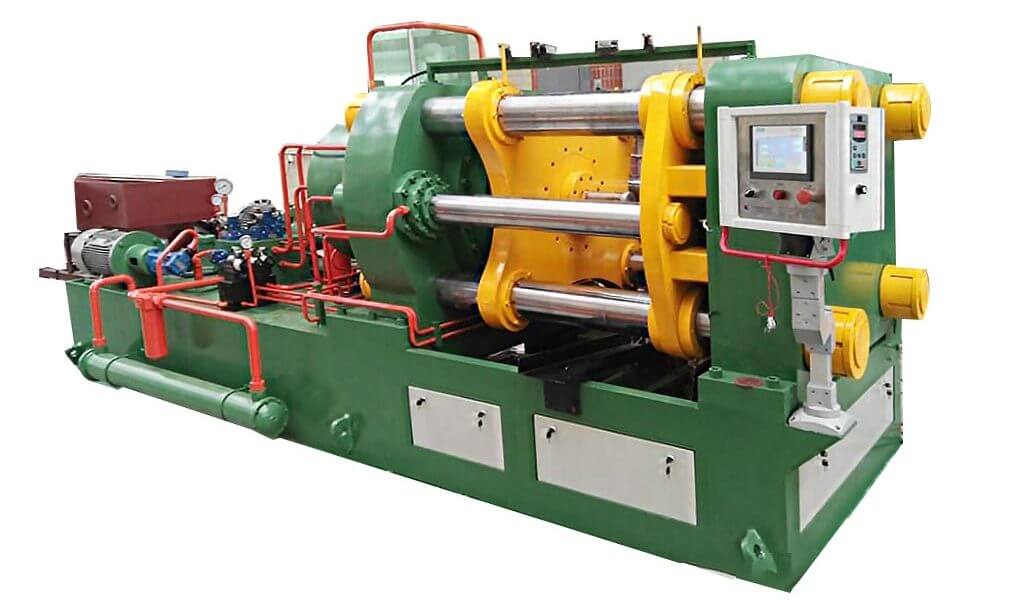
CDOCAST CDO-EX250T to CDO-EX800T metal extrusion machines use a four-column horizontal hydraulic structure to extrude prepared billets into rod, wire and approved solid profiles. Five models cover 250–800 tons of thrust and published billet sizes from Φ40×140 mm to Φ80×150 mm.
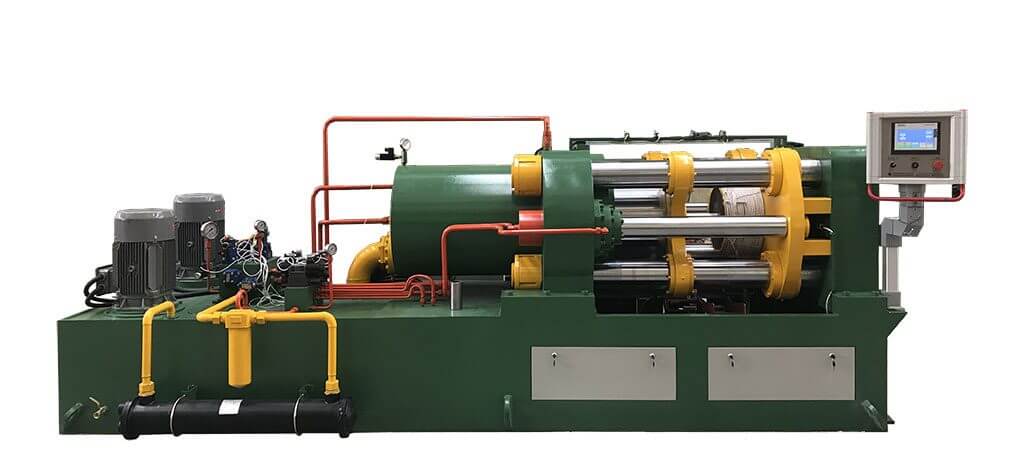
A metal extrusion machine—also called a hydraulic metal extrusion press or metal extruder—forces a prepared billet through a shaped die. The die opening determines the cross-section of the emerging rod, wire or solid profile, while billet alloy, temperature, lubrication, extrusion ratio and cooling determine the achievable surface and dimensional result.
This CDOCAST series is a billet-fed horizontal hydraulic extrusion press. The term “continuous extrusion” on the original product page refers to successive billet production and billet-to-billet process continuity; it should not be confused with a rotary CONFORM-type continuous extrusion machine. The practical production arrangement must be selected from the customer's alloy, billet and finished-product drawing.
Selecting a larger tonnage is not automatically better. The correct model depends on alloy flow stress, billet diameter, extrusion ratio, die geometry and the required final section.
Entry model for smaller approved nonferrous billets and product sections. Its published billet size is Φ40×140 mm.
For a larger Φ50×150 mm billet envelope where the application requires more thrust than the 250T configuration.
Mid-range 500T machine with a published Φ60×150 mm billet size for approved copper, silver and nonferrous extrusion projects.
Uses the same published 150 mm billet length and 11 kW main motor as the 500T model, with a Φ70 mm billet diameter and higher thrust.
Largest standard configuration in this series, with Φ80×150 mm billet size, 22 kW main motor and higher listed forward and return speeds.
Published specifications for all five CDO-EX models. On mobile, swipe the table horizontally to compare every model.
| Specification | CDO-EX250T | CDO-EX350T | CDO-EX500T | CDO-EX600T | CDO-EX800T |
|---|---|---|---|---|---|
| Maximum thrust | 250T | 350T | 500T | 600T | 800T |
| Voltage | 380 V | 380 V | 380 V | 380 V | 380 V |
| Maximum pressure | 22 MPa | 25 MPa | 24 MPa | 24 MPa | 31.5 MPa |
| Billet size | Φ40×140 mm | Φ50×150 mm | Φ60×150 mm | Φ70×150 mm | Φ80×150 mm |
| Main cylinder length | 450 mm | 450 mm | 500 mm | 500 mm | 650 mm |
| Forward speed | 150 mm/s | 150 mm/s | 150 mm/s | 150 mm/s | 200 mm/s |
| Withdraw speed | 200 mm/s | 200 mm/s | 200 mm/s | 200 mm/s | 250 mm/s |
| Main motor power | 7.5 kW | 11 kW | 11 kW | 11 kW | 22 kW |
| Total installed power | 14 kW | 19 kW | 30 kW | 30 kW | 32 kW |
| Machine dimensions (L×W×H) | 4000×1500×1400 mm | 4200×1500×1400 mm | 5000×1600×1600 mm | 5000×1600×1600 mm | 5500×1800×1600 mm |
| Machine weight | 4000 kg | 4500 kg | 6000 kg | 7000 kg | 8000 kg |
Published forward and withdraw values are machine movement speeds, not guaranteed finished-product output. Actual extrusion speed and capacity depend on alloy, billet temperature, extrusion ratio, die, cooling, handling and quality requirements. Confirm local power frequency, phase, transformer capacity and foundation conditions before ordering.
A stable metal extrusion line needs controlled billet preparation, die setup, extrusion and downstream handling—not only sufficient press tonnage.
Confirm alloy, billet diameter and length, incoming condition, finished cross-section, tolerance and required production rate.
Clean and prepare the billet. Set the alloy-specific billet, container and die conditions established by the production process.
Load the billet and verify alignment between the ram, container, front die head and downstream guide path.
The ram builds controlled pressure and pushes metal through the selected die to form rod, wire or an approved solid profile.
Guide, cool, straighten, cut or coil the extrusion as required, then inspect section size, surface, straightness and defects.
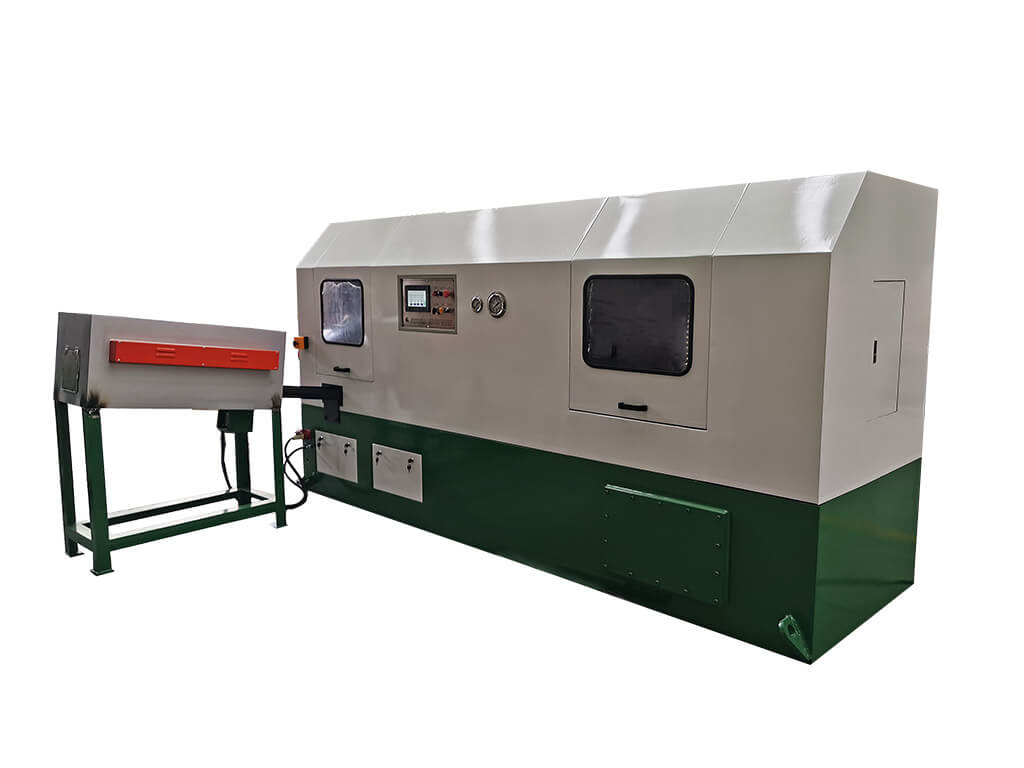
The design combines a rigid horizontal frame, controlled hydraulic movement and accessible front die handling.
Feasibility depends on the exact alloy, billet quality, extrusion ratio, tooling and required section—not only the material name.
Send engineering data with the inquiry so CDOCAST can evaluate thrust, billet size, die design and downstream line requirements together.
Internal links help buyers plan the processes before and after billet extrusion without turning this product page into a general buyer guide.
View the dedicated CDO-EX250T to CDO-EX800T parameter sheet and published equipment overview.
Direct answers for buyers comparing copper rod extrusion machines and hydraulic nonferrous extrusion presses.
The published applications include copper and copper alloys, silver, aluminum alloys, zinc and other nonferrous metals. Final feasibility depends on the exact alloy, billet condition, extrusion ratio, die geometry, temperature control and required product tolerance.
It is a billet-fed horizontal hydraulic extrusion press. Successive billet operation can support production continuity, but it is not the same machine principle as a rotary CONFORM-type continuous extrusion system. Send the required product length, coil plan and joint requirement so the production route can be evaluated correctly.
Do not select only by tonnage. Provide the alloy, billet diameter and length, finished cross-section, extrusion ratio, tolerance and production target. These inputs determine whether the available thrust, billet envelope, die design and installed power are suitable.
It can extrude approved solid rod, wire feedstock and profiles through dedicated dies. Very small finished wire is usually obtained through downstream wire drawing rather than expecting the extrusion press alone to reach final fine-wire size.
The published table lists 380 V for all five standard models. Confirm local phase, frequency, transformer capacity and electrical standard before production because site requirements may differ.
Output depends on alloy, billet size and temperature, extrusion ratio, ram cycle, die design, cooling, billet handling, cutting or coiling, inspection and planned downtime. The listed forward speed is a machine movement value and should not be treated as guaranteed product output.
Die scope should be defined from each finished-product drawing. Different rod diameters and profile cross-sections normally require dedicated tooling, and additional dies should be listed separately in the technical and commercial proposal.
Send the alloy and composition, billet drawing, finished product drawing, extrusion ratio if known, target output, delivery form, cooling and downstream process, die quantity, factory voltage and available floor space. This allows CDOCAST to evaluate the machine model and complete line scope.
Send your billet specification, finished-product drawing, alloy and required output for CDO-EX model and die evaluation.