Progressive die for gold silver coins
Why We Do Not Recommend Progressive Dies for Gold and Silver Coins
A progressive die or compound die can cut and stamp in one stroke, but it is usually not the best choice for high-quality gold coins, silver coins, minted bars or collector medals. The main problem is not only die cost. It is surface quality, relief sharpness, burr control, die safety and long-term production stability.
What is a progressive die in coin and bar production?
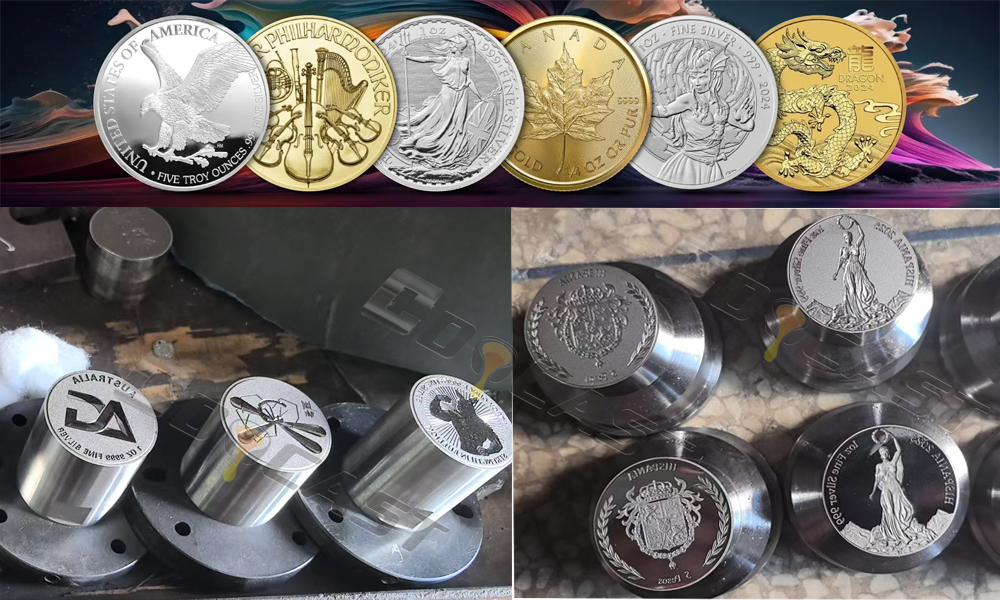
In precious metal minting, some buyers ask whether one die can punch the blank and stamp the design at the same time. This type of tooling is often called a progressive die, compound die or combined blanking and stamping die. In one press stroke, the strip is cut and the design is stamped directly onto the part.
For investment coins, proof-like coins, fine medals and minted gold or silver bars, the blank must usually be cut, cleaned, polished and annealed before final minting. Removing those steps may save handling time, but it also removes the preparation that makes the final surface bright, sharp and stable.


Standard process for high-quality gold and silver coin minting
Professional gold silver coin minting normally separates blank preparation from final striking. Each machine works on one controlled step, which makes quality easier to control and troubleshooting much simpler.
Why the two-step method gives better surface and relief
Gold and silver are soft compared with many industrial metals, but premium coin minting still requires controlled metal flow. When a blank is annealed before minting, its internal stress is reduced and the material fills the fine details of the coin die more evenly. This is especially important for deep relief, small lettering, logos, serial marks and mirror-like background surfaces.
With a progressive die, the blank is cut and stamped before proper surface preparation. Cutting marks, strip stress and tiny burrs remain on the material. The result is often a shallower pattern, weaker relief, less stable edge quality and a surface that cannot reach the same finish as a separately prepared blank.

Main problems when using progressive dies for gold and silver coins
1 Lower pattern sharpness
Without annealing before minting, the blank is harder and less willing to flow into fine die details. Relief depth, small text and logo edges can become weaker.
2 Burrs and edge flash
Because cutting and stamping happen inside one die set, metal can be squeezed toward the edge. After die wear, burrs and uneven edges become more obvious.
3 Limited product size
Progressive dies are more suitable for small and simple parts. For larger coins, detailed medals or minted bars, die stress and product deformation risks increase.
4 Higher die damage risk
In automatic production, strip feeding error, blank jamming or an empty stroke can damage the punch and die. One tooling failure may stop the complete line.
5 Strict strip requirements
Long precious metal strip must have stable thickness, width and straightness. If the strip is not accurate, feeding position and stamping quality become unstable.
6 Difficult quality correction
When cutting and stamping are combined, it is harder to identify whether a defect comes from strip preparation, cutting clearance, die wear or press setting.
Progressive die vs standard blanking and minting process
| Production method | Suitable use | Main advantage | Main limitation |
|---|---|---|---|
| Progressive die / compound die | Small simple pieces, low relief medals, basic promotional tokens | Cutting and stamping can be combined in one stroke | Surface quality, burr control and die safety are harder to maintain |
| Hydraulic punching + blank treatment + hydraulic minting press | Gold coins, silver coins, minted bars, proof-like pieces and investment bullion | Better surface finish, relief detail, process control and repeatability | Requires more process steps and matched equipment |
When can a progressive die still be considered?
A progressive die is not completely wrong in every case. It can be discussed only when the product is small, simple and not positioned as a premium bullion coin or mirror-finish minted product.
For high-quality bullion coins, collector coins, mirror-surface medals or minted investment bars, CDOCAST still recommends the standard blanking, blank treatment and hydraulic minting process.
Recommended CDOCAST equipment for a stable minting process
The right equipment combination depends on coin size, bar size, pattern depth, target surface, daily output and whether the production line needs manual, semi-automatic or automatic handling.
FAQ about progressive dies for gold and silver coin minting
Can one die cut and stamp gold coins at the same time?
Yes, a progressive die or compound die can combine blanking and stamping, but it is not recommended for high-quality gold and silver coins because the blank cannot be properly polished and annealed before final minting.
Why do coin blanks need annealing before minting?
Annealing reduces internal stress and improves metal ductility. A softer, prepared blank flows better into the minting die, which helps produce sharper relief, cleaner lettering and a more stable surface.
Why do progressive dies create burrs or edge flash?
Cutting and stamping happen in the same die set. As die clearance changes from wear, metal can be squeezed toward the edge and form burrs. This is a serious issue for precious metal coins and minted bars.
What is the better process for premium gold and silver coins?
The better process is separate blanking, blank polishing or cleaning, annealing, and final minting with a hydraulic press and custom coin minting die.
Is a progressive die cheaper in the long term?
Not always. Although it may reduce one handling step, it can increase die damage risk, burr repair cost, product rejection and downtime. For premium bullion products, the standard two-step process is usually more reliable.
Need help choosing coin minting dies or a complete minting line?
Send CDOCAST your coin size, material, thickness, target design depth, daily output and surface requirement. We can recommend the correct blanking tool, annealing furnace, hydraulic press and custom minting die setup.