
CDO-HBM1 Small-Size Bead Making Machine
For fine hollow jewelry beads from Φ2 mm to Φ6 mm. Select the model when the product plan is centered on smaller bead-chain and decorative component sizes.
Bead rangeΦ2–6 mm
Speed3400/hour
Motor3 kW
 cdocast
Buy The Most Popular Hollow Ball Making Machine In The Market
CDOCAST CDO-HBM1 and CDO-HBM2 form prepared hollow metal tube into 2–10 mm hollow balls and jewelry beads. Dedicated tooling can be selected for round beads and other approved bead profiles, with a published production speed of up to 3400 beads per hour.
A hollow ball making machine—also called a hollow bead making machine—uses matched forming dies to shape prepared hollow metal tube into lightweight jewelry beads. It is used for gold, K-gold, silver, copper and compatible alloys when manufacturers need the appearance and volume of a solid bead with lower metal weight.
The machine does not produce hollow tube from raw sheet and it does not automatically remove a poor tube weld. The incoming tube must already have the correct outside diameter, wall thickness, roundness, weld quality and material condition. The bead tooling then controls the finished diameter and profile. Polishing or another finishing step is normally required after forming.
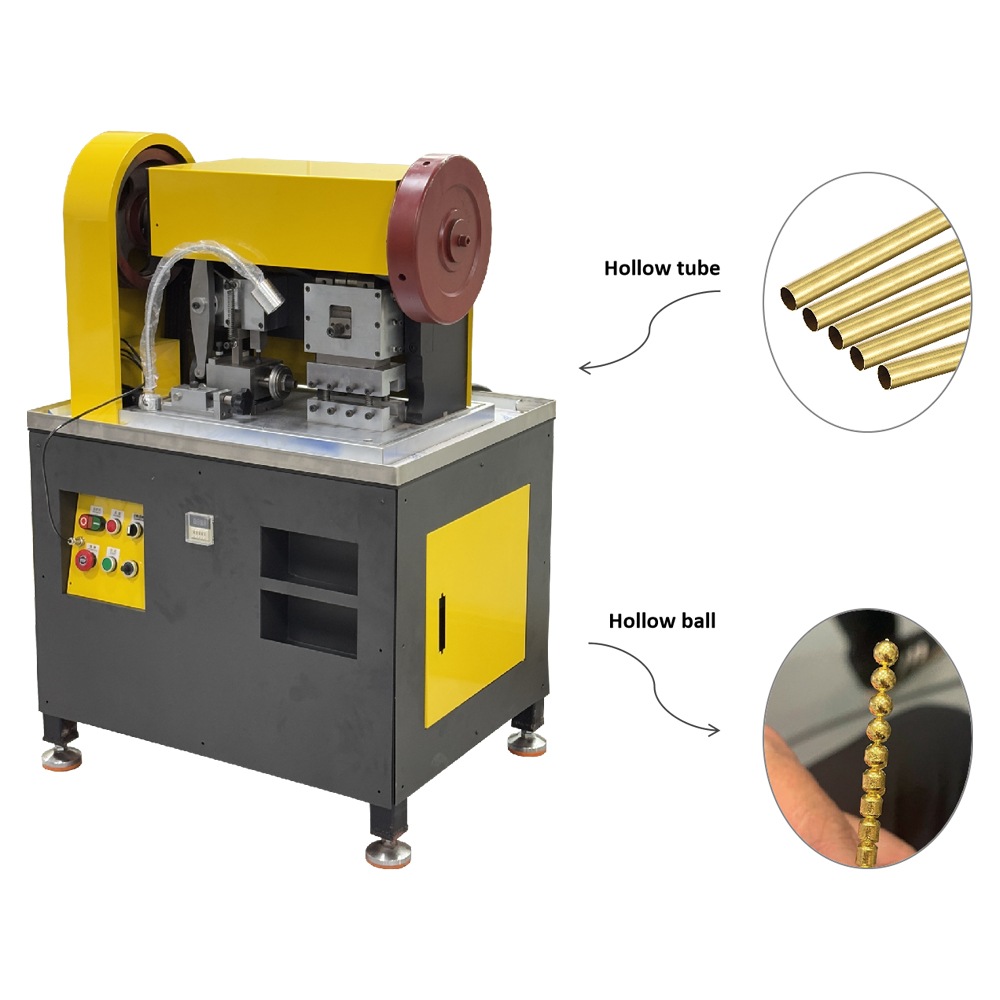
The machines share the same listed power, speed, size and weight. The main model difference is the supported bead-diameter range and matched tooling.
For fine hollow jewelry beads from Φ2 mm to Φ6 mm. Select the model when the product plan is centered on smaller bead-chain and decorative component sizes.

For larger hollow jewelry beads from Φ6 mm to Φ10 mm. Select it for bead products that exceed the working range of CDO-HBM1.
Published specifications for CDO-HBM1 and CDO-HBM2, cross-checked with the CDOCAST Bead Forming Series.
| Specification | CDO-HBM1 | CDO-HBM2 |
|---|---|---|
| Published machine type | Small Size Bead Making Machine | Large Size Bead Making Machine |
| Voltage | 380 V, 3 phase, 50 Hz | 380 V, 3 phase, 50 Hz |
| Motor power | 3 kW | 3 kW |
| Bead diameter | Φ2–6 mm | Φ6–10 mm |
| Published bead-making speed | 3400 beads/hour | 3400 beads/hour |
| Machine size (L×W×H) | 650×600×1230 mm | 650×600×1230 mm |
| Machine weight | 600 kg | 600 kg |
Actual output depends on tube dimensions, alloy condition, bead profile, tooling, feeding stability, inspection and downstream finishing. Confirm the destination electrical standard before production.
The hollow ball machine is the central forming step, but stable production starts with suitable tube and ends with controlled finishing.
Produce or purchase tube with the required alloy, outside diameter, wall thickness, roundness and weld quality.
Set the material condition for forming, then inspect tube straightness, seam and dimensions before feeding.
Fit the die set selected for bead diameter, profile, tube dimensions and required neck or separation geometry.
The machine advances the tube through the forming area and shapes consecutive bead sections under the matched tooling.
Separate beads as required, then deburr, clean, grind or polish them to the specified finished appearance.
Most production problems come from mismatched tube and tooling rather than from nominal bead diameter alone.

Final shape availability depends on dedicated tooling and approval of the customer's tube and bead sample.

A complete gold or silver hollow bead line can include melting, strip rolling, slitting, hollow tube forming and welding, tube sizing, bead forming and final polishing. The exact route depends on whether the factory starts from raw metal, strip or finished hollow tube.
Send the tube specification and finished bead drawing together so the machine model and tooling can be evaluated correctly.
Practical answers for jewelry factories comparing hollow gold and silver bead equipment.
The direct input is prepared hollow metal tube—not raw metal sheet. The tube must match the required bead and die dimensions and should have suitable wall thickness, roundness, weld quality and material condition.
CDO-HBM1 covers the published Φ2–6 mm range, while CDO-HBM2 covers Φ6–10 mm. Tooling must be selected for the actual bead diameter and profile.
Yes. The published applications include gold, K-gold, silver and copper. Provide the exact alloy because forming behavior and annealing requirements vary by purity and composition.
Normally no. Different diameters and profiles generally require dedicated dies. Round, oval, teardrop and abacus-style beads should be evaluated from a drawing or sample before tooling is produced.
The bead machine forms prepared hollow tube. If the tube was produced by strip forming and welding, its seam quality depends on the upstream tube process; the bead machine does not automatically eliminate a poor weld seam.
It is the published machine speed for both models. Actual output depends on tube dimensions, alloy condition, bead geometry, tooling, feeding stability, quality inspection and the required finishing process.
A line starting from raw precious metal can include a melting furnace, rolling mill, slitting machine, hollow tube forming and welding machine, annealing or tube sizing equipment, hollow bead making machine and jewelry polishing machine.
Provide the alloy, tube outside diameter and wall thickness, finished bead drawing, required sizes and profiles, production target, die quantity, factory voltage and whether upstream tube-making or downstream polishing equipment is required.
Send CDOCAST your tube specification, finished bead drawing, alloy and production target for CDO-HBM1, CDO-HBM2 and forming-die selection.