Φ180×200 mm MOV backup rolls support the Φ40×200 mm DC53 work rolls for thin-strip reduction.
 cdocast
- Call Us: 008615168765707
- Mail Us: sales@cdocast.com
cdocastBuy the Most advanced Sheets Rolling Mill For Types Of Metals Strip
The CDOCAST 15HP CNC four-roller ultra-thin sheet rolling mill combines MOV backup rolls, DC53 work rolls, twin servo downfeed, variable-frequency speed control and synchronized payoff/take-up units. It is configured for metal strip from 0.2 mm down to 0.004 mm with a maximum rolling width of 150 mm.

A CNC 4-roller precision rolling machine uses smaller work rolls supported by larger backup rolls. The backup rolls reduce work-roll deflection under load, while the servo lift controls the roll-gap adjustment. This arrangement is used when a two-high mill cannot provide the required thin-gauge stability or thickness consistency.
This 15HP CNC four-high rolling mill is intended for controlled ultra-thin finishing passes. Incoming thickness, strip width, alloy hardness, annealing schedule, pass reduction and winding tension still need to be confirmed before production.
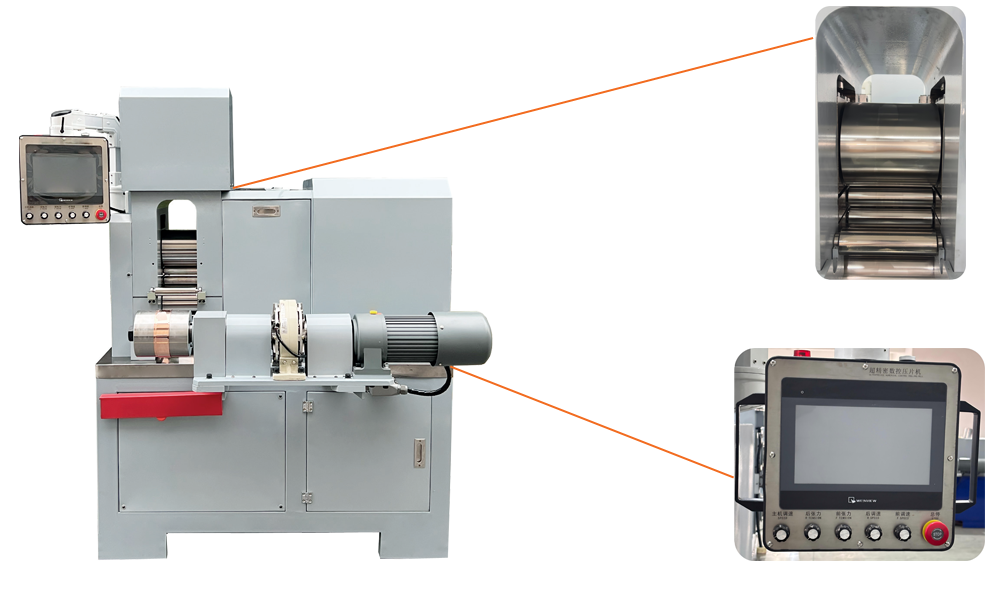
Core mechanical and control functions of the single 15HP ultra-thin sheet rolling configuration.
Φ180×200 mm MOV backup rolls support the Φ40×200 mm DC53 work rolls for thin-strip reduction.
The 15HP main motor includes variable-frequency speed regulation for controlled rolling operation.
Two 3HP servo motors control the downfeed system for repeatable four-high roll-gap adjustment.
Two 1HP winding motors with magnetic powder clutches manage strip feeding and collection.
Complete specification of the single 15HP four-roller ultra-thin sheet rolling machine.
| Specification | 15HP Four-Roller Ultra-Thin Sheet Rolling Mill |
|---|---|
| Machine dimensions (L×W×H) | 1700×1300×1900 mm |
| Machine weight | 1800 kg |
| Backup rolls | MOV alloy steel, Φ180×200 mm wide |
| Work rolls | DC53 tool steel, Φ40×200 mm wide |
| Main motor | 15 HP with variable-frequency drive speed control |
| Downfeed servo motors | Two sets, 3 HP each |
| Payoff and take-up motors | Two sets, 1 HP each, with magnetic powder clutches |
| Automatic lubrication | 2 L automatic oil-pump system |
| Rolling thickness | 0.2–0.004 mm |
| Maximum rolling width | 150 mm |
| Machine voltage | 380 V |
| Power cable | 5-core, 6 mm² |
Functions that must be matched as one production system rather than selected from motor power alone.
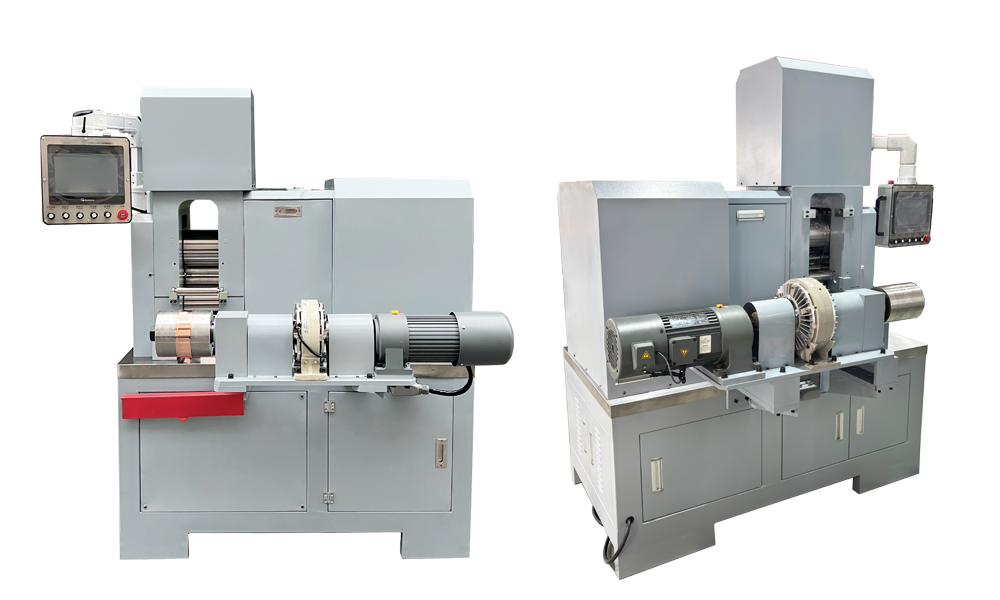
The CNC operating interface works with two 3HP servo motors to control the downfeed system and repeatable roll-gap adjustment.
Φ180×200 mm MOV backup rolls support the Φ40×200 mm DC53 work rolls for the 0.2–0.004 mm ultra-thin rolling range.
Two 1HP winding motors with magnetic powder clutches control material feeding and strip collection, while the 2 L automatic oil pump supports continuous lubrication.
A practical sequence for protecting the precision roll system and controlling the final gauge.
Complete larger reduction passes, edge inspection and alloy-specific annealing before precision finishing.
Enter a controlled reduction sequence based on metal, width, incoming gauge and required final thickness.
Monitor roll gap, strip behavior and coiler tension through the final passes; verify thickness with suitable measuring equipment.
For larger primary reductions, compare the metal strips rolling mill. For carbide-roll final finishing, review the tungsten carbide rolling mill.
Review the 15HP four-high ultra-thin sheet rolling machine together with other CDOCAST rolling equipment.
Technical answers about the single 15HP ultra-thin sheet rolling configuration.
It is a four-high rolling mill with smaller work rolls supported by larger backup rolls, combined with CNC operation and servo roll-gap adjustment. The configuration is used for controlled thin-strip and foil finishing where roll deflection and thickness consistency are important.
The specified rolling thickness range is 0.2–0.004 mm, with a maximum strip width of 150 mm. Actual production should be confirmed against the alloy, incoming gauge, strip condition and reduction schedule.
The machine uses Φ180×200 mm MOV alloy-steel backup rolls and Φ40×200 mm DC53 tool-steel work rolls. The larger rolls support the smaller work rolls during ultra-thin reduction.
The 15HP main motor is equipped with a variable-frequency drive so the operating speed can be adjusted for the material and pass schedule.
Two 3HP servo motors control the downfeed system. They work with the CNC interface to provide repeatable roll-gap adjustment during precision rolling.
Yes. The specified configuration includes two 1HP winding motors with magnetic powder clutches—one set for payoff and one set for take-up—to control strip feeding and collection.
The machine uses an automatic lubrication system with a 2 L oil pump to supply the rolling mechanism during operation.
The machine voltage is 380 V. The specified incoming power cable is a 5-core cable with a 6 mm² conductor cross-section.
Send your metal, incoming thickness, target thickness, strip width and required production rate so CDOCAST can evaluate the rolling and annealing sequence.
Contact CDOCAST