How to Make 1g-100g Gold Silver Bars
CDOCAST Buyer Guide
How to Make 1g-100g Gold and Silver Bars with a Complete Minting Line
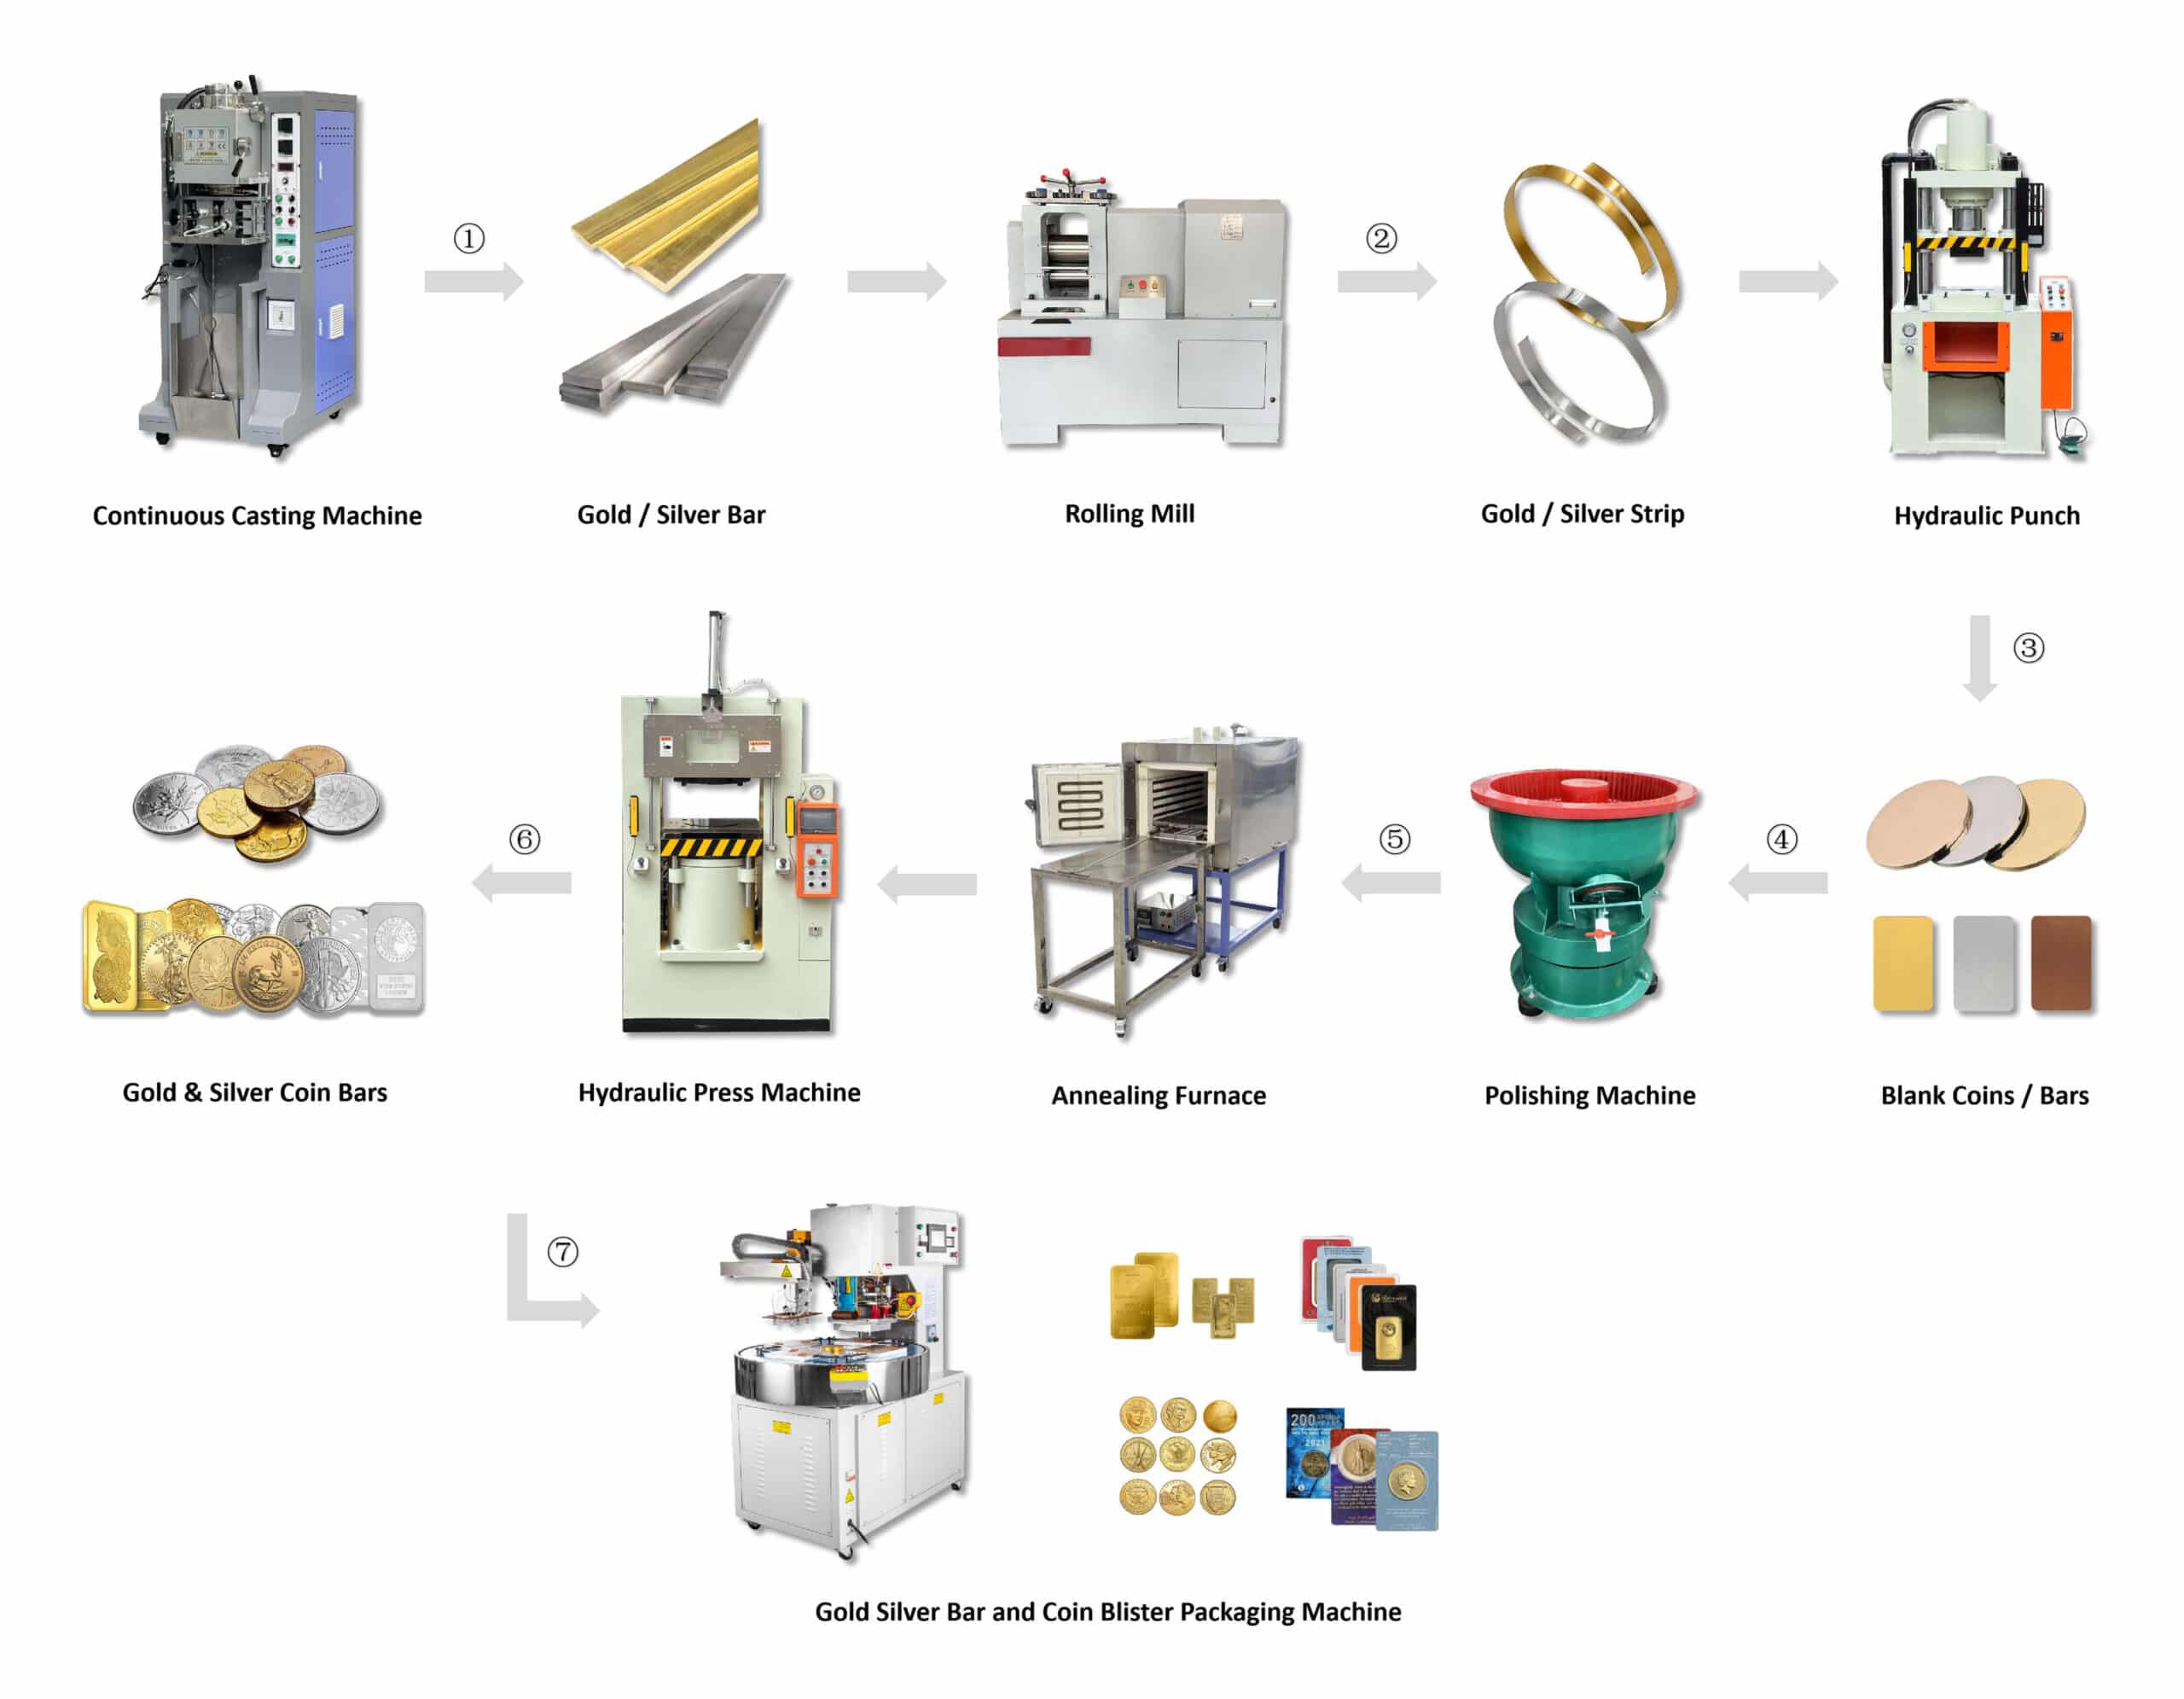
For 1g-100g gold and silver bars, the best production route is usually not simple open casting. A stable line uses melting or continuous casting for dense strip, precision rolling for thickness control, blanking for weight accuracy, hydraulic minting press for logo stamping, then polishing, inspection and packaging.
Short Answer
The Practical Way to Produce 1g-100g Gold Silver Bars
Use a continuous casting machine to make dense precious metal strip, roll the strip to the required thickness, punch each blank to a controlled weight, then use a hydraulic minting press with custom bar dies to stamp the logo and final surface.
- For small trial production, a medium frequency melting furnace can be used before rolling and stamping.
- For stable factory output, continuous casting is better because strip density and thickness are easier to control.
- For 1g-20g small bars, a 100 ton hydraulic press gives enough pressure reserve and protects the dies.
- For 50g-100g bars, a 300 ton hydraulic press gives better edge definition, deeper relief and flatter surface.
Process Flow
1g-100g Gold Silver Bar Production Process
Melting or Continuous Casting
Prepare dense gold or silver strip with fewer pores and better structure.
Precision Rolling
Roll the strip to target thickness before blanking.
Blanking
Punch 1g-100g blanks according to target weight and size.
Minting Press
Stamp logo, text, weight, purity and pattern with custom dies.
Polishing and Packaging
Clean, inspect, weigh and package finished gold or silver bars.
Equipment Strategy
Core Equipment for a 1g-100g Gold Silver Bar Minting Line

Gold Melting Furnace
Entry-level choice for small batches, trial orders and flexible multi-size production.

Continuous Casting Machine
Recommended for stable production because dense strip improves rolling, blanking and minting results.
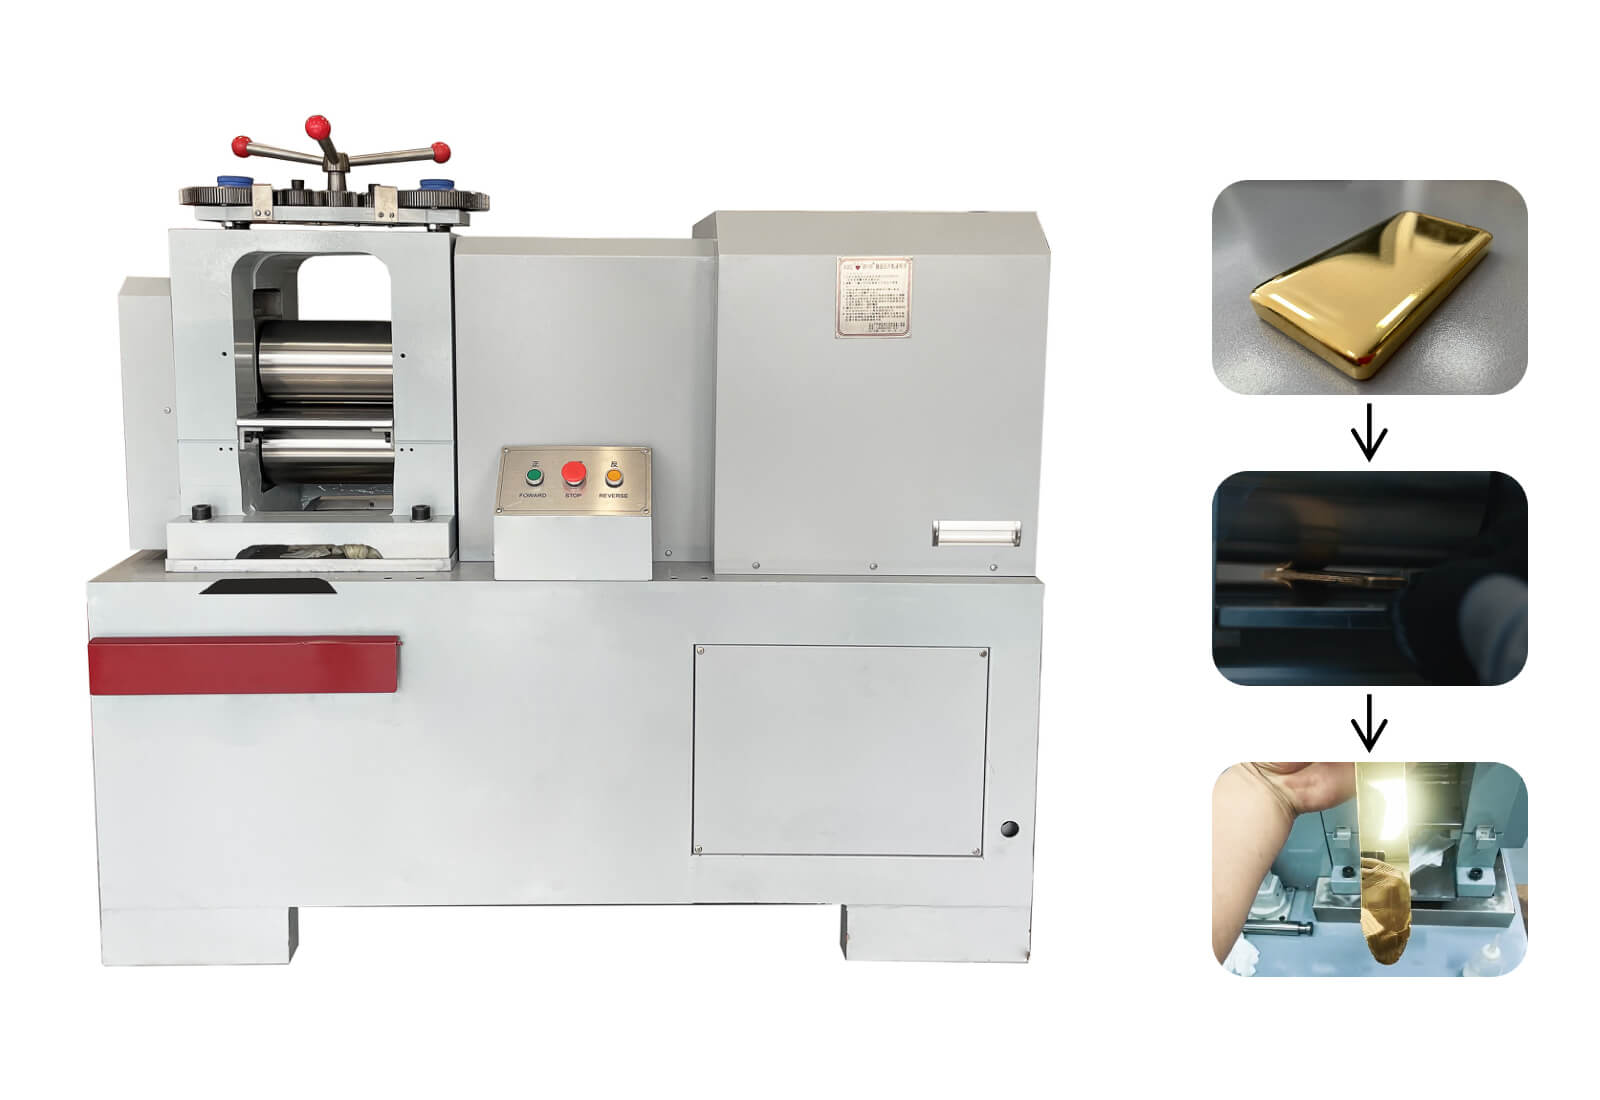
Precision Rolling Mill
Controls strip thickness before blanking, helping reduce weight deviation in small bars.
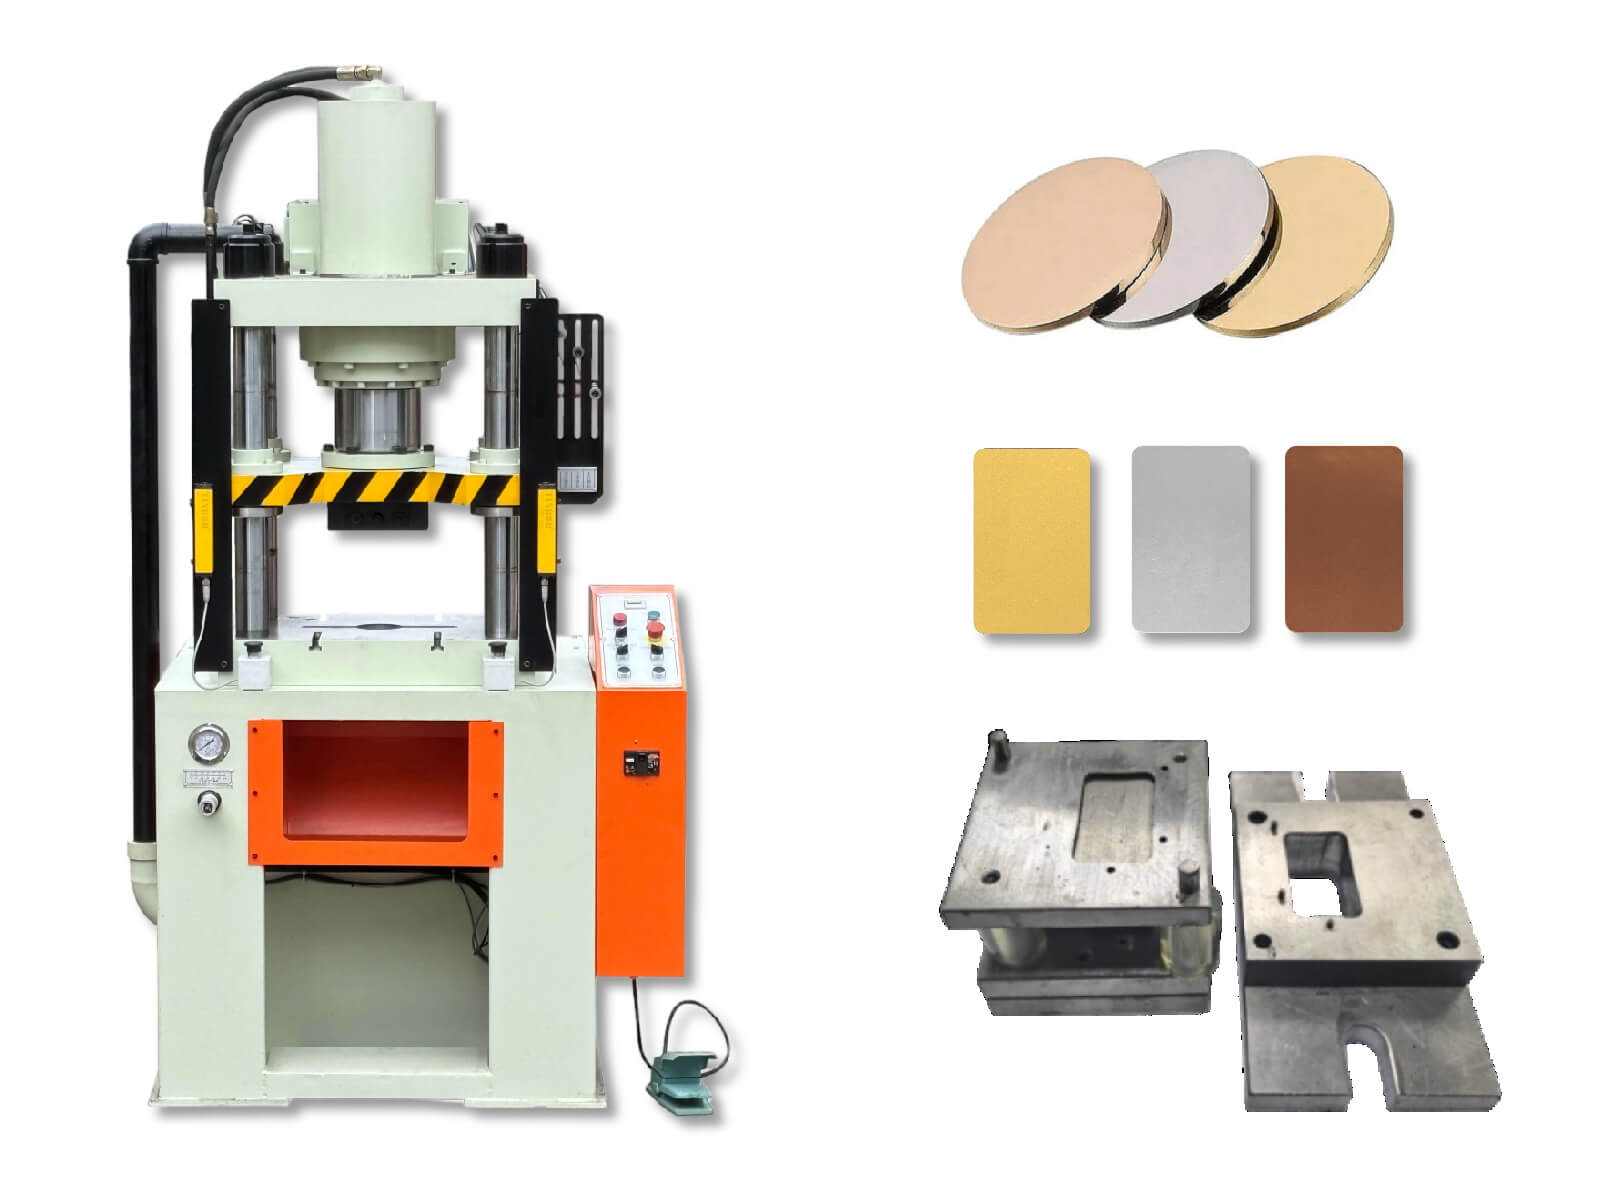
Hydraulic Punching Machine
Punches gold or silver strip into accurate blanks for 1g, 5g, 10g, 50g and 100g bars.

Hydraulic Minting Press
Stamps sharp logo, text, serial area, purity mark and decorative pattern with custom dies.

Bar Packaging Machine
Protects finished bars from fingerprints, oxidation and handling damage before sale.
Minting Press Selection
Why 1g and 100g Bars Should Not Always Use the Same Hydraulic Press
A 1g gold bar needs much less forming pressure than a 100g bar. If a normal 300 ton hydraulic press is used for 1g bars, the starting oil pressure and heavy press structure can be too aggressive for the small die set. This increases the risk of die damage and also makes every small-bar die set more expensive.
Use 100 Ton for 1g-20g Bars
Better for 1g, 2.5g, 5g, 10g and 20g bars because the pressure range and die size are more suitable.
- Lower starting hydraulic pressure is easier to control.
- Small logo dies are less likely to be damaged by excessive impact.
- Die holder, mold base and tooling material are smaller, so die cost is lower.
Use 300 Ton for 50g-100g Bars
Better for larger gold and silver bars because the stamping area and metal flow demand are much higher.
- Larger frame and platen support bigger bar dies.
- Higher tonnage fills wide logo fields and deep relief patterns.
- Finished bars have cleaner edges, stronger details and more stable thickness.
If One Press Must Cover 1g-100g
Choose a servo hydraulic press. Servo control gives more accurate pressure adjustment, especially at low pressure for 1g small bars, while still providing enough force for 50g-100g bars. Without servo control, using a large 300 ton press for 1g bars can waste tooling material, increase mold base cost and make small dies easier to damage.
Decision Table
Equipment Choice by Production Goal
| Production Goal | Recommended Equipment | Why It Matters |
|---|---|---|
| Small batch 1g-20g bars | Melting furnace, rolling mill, punching machine, 100 ton press, bar dies | Lower investment, flexible size change, suitable for trial orders and brand testing. |
| Stable 1g-100g production | Continuous casting machine, precision rolling mill, punching machine, 100 ton + 300 ton presses | Better strip density, more stable blank weight and better stamping quality across different bar sizes. |
| Premium mirror finish bars | High quality dies, stable hydraulic press, polishing and cleaning line, protective packaging | Improves logo clarity, surface appearance and final retail presentation. |
| High output factory line | Automatic feeding, weighing and sorting, polishing, packaging and inspection system | Reduces labor, rejects overweight/underweight blanks and improves repeatability. |
Quality Control
Key Points That Decide Finished Gold Silver Bar Quality
Strip Density
Pores or loose structure in the strip can cause weak surfaces, cracks or uneven flow during minting.
Thickness Accuracy
Stable rolling thickness makes blank weight easier to control, especially for 1g and 5g bars.
Blank Weight
Each blank should be checked before stamping to avoid overweight or underweight finished bars.
Die Quality
Good minting dies decide logo depth, edge definition, mirror field and repeated production stability.
Press Tonnage
Insufficient pressure causes incomplete pattern filling. Excessive pressure can increase die wear.
Packaging Protection
Finished bars need clean handling and packaging to avoid fingerprints, oxidation and scratches.
Complete Line Options
Auxiliary Equipment for a Professional Gold Silver Bar Line
FAQ
1g-100g Gold Silver Bar Production FAQ
What is the best method for making 1g-100g gold and silver bars?
For investment-grade small bars, minting is usually better than simple casting. The common route is continuous casting or melting, rolling, blanking, hydraulic pressing with dies, polishing, inspection and packaging.
Why is continuous casting recommended before rolling and minting?
Continuous casting can produce dense and uniform precious metal strip. Better strip quality reduces rolling defects, blanking weight variation and stamping defects.
Can one hydraulic press make all 1g-100g bars?
One press can cover some ranges, but for a complete 1g-100g line, a 100 ton press for small bars and a 300 ton press for 50g-100g bars is more stable and protects die life.
What equipment is needed for accurate blank weight?
A precision rolling mill controls strip thickness, a punching machine cuts blanks, and an automatic weighing system checks each blank before minting.
Do gold and silver bars need polishing before packaging?
Yes, polishing or cleaning removes oil, dust and handling marks. Clean bars should be packaged quickly to avoid fingerprints and surface oxidation.
Need a 1g-100g Gold Silver Bar Production Line?
Send your target bar sizes, daily output, logo design, purity mark, packaging style and budget range. CDOCAST can recommend the melting, casting, rolling, blanking, minting and packaging configuration.